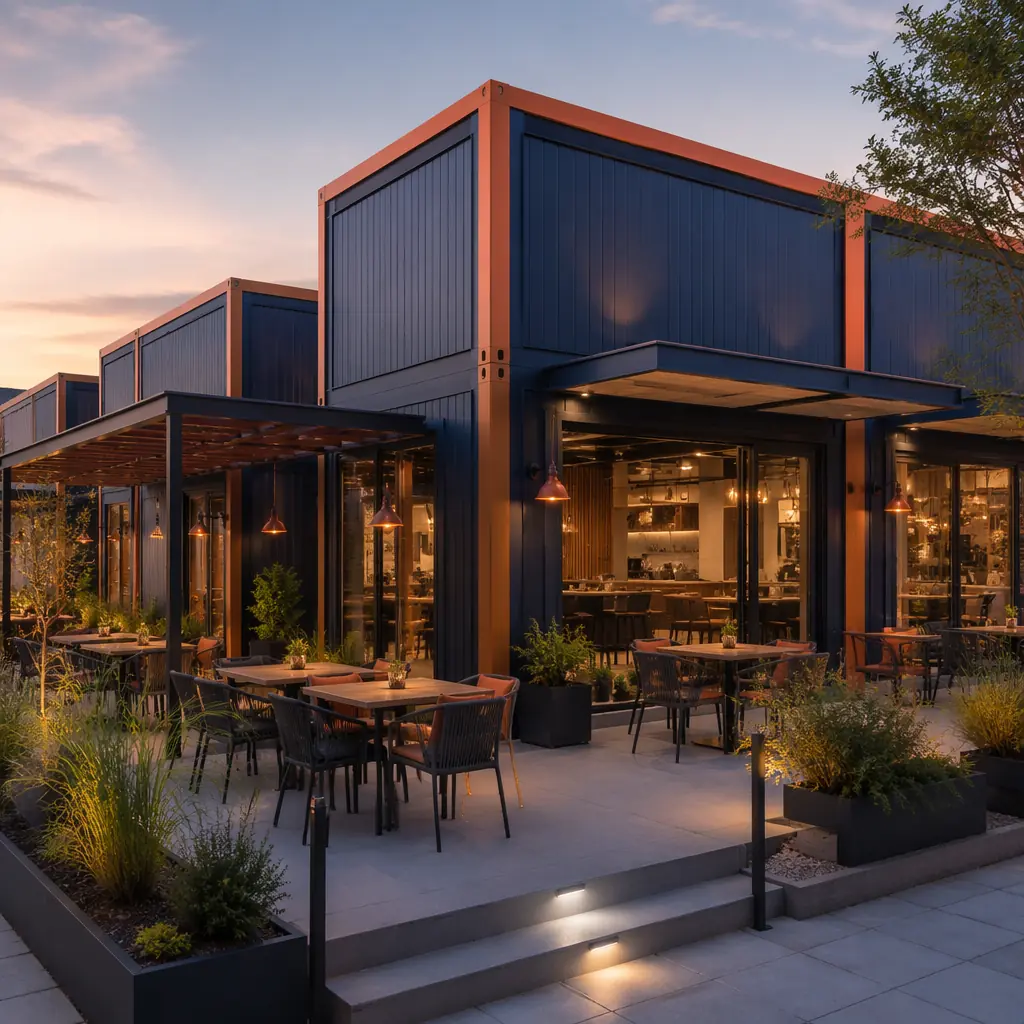
Restaurant construction is a race against carrying costs. Every month a restaurant site sits under construction is a month of lease payments, management overhead, and zero revenue from a location that was supposed to open last quarter. For franchise operators scaling from 5 to 50 locations, the math is unforgiving: a 6-month delay on a $1.2 million build-out burns $180,000 in lease and overhead before the first customer walks through the door, assuming a $30,000/month blended carry cost. Modular construction changes this equation by delivering code-compliant restaurant modules, with integrated commercial kitchens, MEP rough-ins, and finished dining areas, in 12–16 weeks from contract to turnover, compared to 24–36 weeks for conventional site-built restaurant construction.
The Restaurant Construction Bottleneck: MEP Coordination
Commercial kitchens are the most MEP-dense spaces in commercial construction outside of hospitals and data centers. A typical 2,000 sq ft restaurant kitchen contains 8–12 plumbing fixtures (hand sinks, prep sinks, 3-compartment sink, mop sink, dishwasher, ice machine, grease trap), 6–10 electrical circuits (refrigeration, cooking equipment, hood controls, fire suppression), HVAC exhaust at 1,200–2,500 CFM through a Type I grease hood, and makeup air at 80% of exhaust volume. Coordinating these systems in a site-built environment requires sequential trade work, plumber, then electrician, then HVAC, then hood installer, with each trade discovering conflicts that force the previous trade to re-work. The result is a 6–8 week MEP rough-in phase where the project stands still for 30% of the time while trades wait for each other.
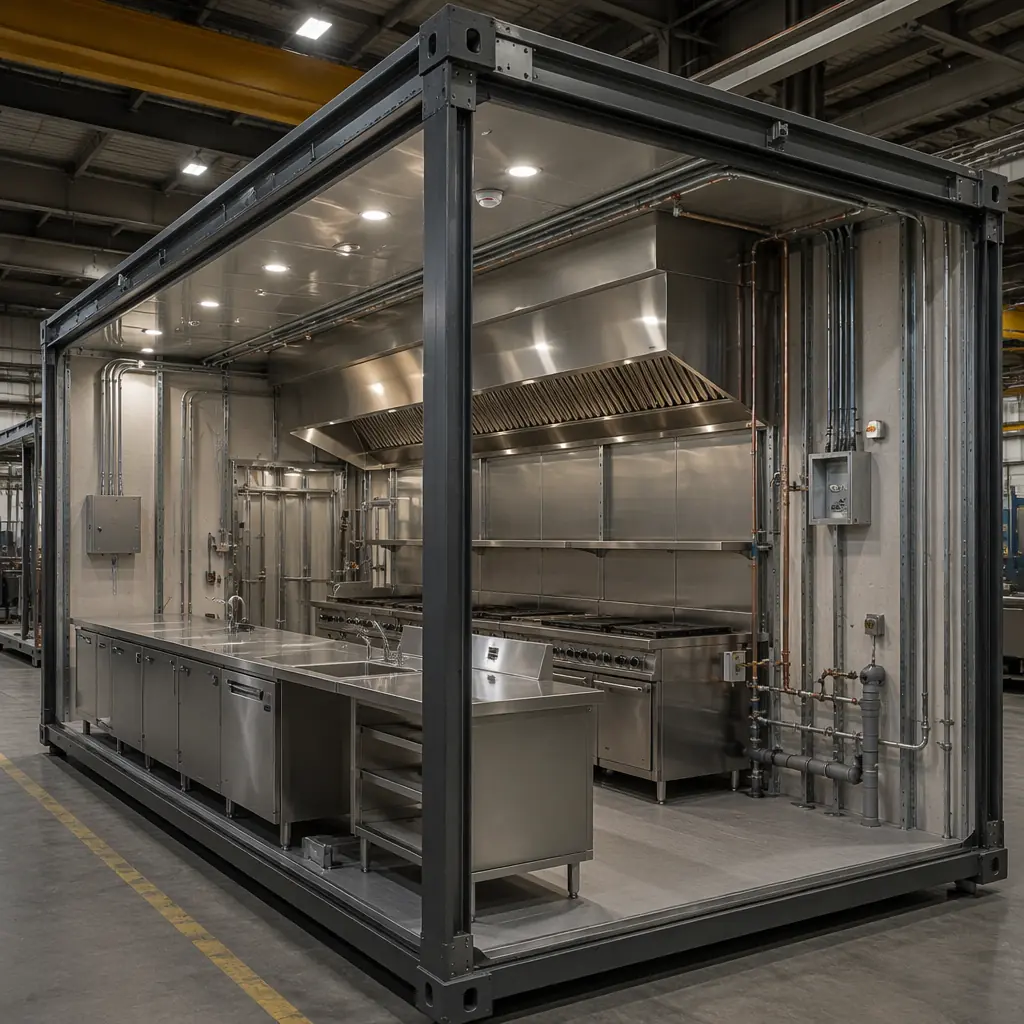
Modular construction eliminates this sequential bottleneck. Kitchen modules are fabricated with all MEP rough-ins installed and coordinated in the factory using a BIM model that resolves every clash before a single pipe is cut. The module ships with plumbing stub-outs labeled for site connection, electrical panels pre-wired to equipment locations, and HVAC ductwork installed to the hood collar. On site, the trades connect to the module, not to each other. For a broader treatment of how modular MEP integration works across building types, our MEP systems guide provides the technical framework.
Health Code Compliance: Factory-Built to NSF Standards
Health department plan review is the single largest source of pre-construction delay for restaurants. A conventional submission goes through 2–4 revision cycles as the health inspector flags issues that the architect didn't anticipate: insufficient hand sink placement, improper floor drain slope, missing indirect waste connections, or wall finishes that don't meet cleanability requirements. Each revision cycle adds 2–3 weeks to the approval timeline.
MODURA's restaurant modules incorporate health code requirements at the design platform level, not the individual-project level:
- Floor surfaces. Factory-installed quarry tile or resinous flooring with 1/8-inch-per-foot slope to floor drains, coved base at all wall-to-floor junctions (6-inch cove, heat-welded seams). This meets NSF/ANSI 2 and FDA Food Code §6-201.11 requirements without the field-installation variability that causes health department rejections.
- Wall finishes. FRP (fiberglass-reinforced plastic) panels or stainless steel sheet up to 48 inches above the floor in all food preparation and warewashing areas, with factory-sealed joints that prevent moisture penetration behind panels, the primary source of mold-related health code violations in site-built kitchens.
- Hand sink placement. Pre-engineered hand sink locations within 25 feet of each food preparation station per FDA Food Code §5-203.11, with factory-installed hot water supply (minimum 100°F per §5-202.12) and indirect waste connections that eliminate cross-connection risks.
- Grease management. Factory-sized and pre-plumbed grease interceptor (typically 1,000–2,000 gallon for full-service kitchens, 500–750 gallon for fast-casual) with accessible cleanout and sample port, located outside the kitchen module but connected via pre-routed waste piping.
For operators navigating the permitting process, our permitting and zoning guide covers how modular construction interacts with local building departments, including the increasingly common pre-approved modular submittal programs that some jurisdictions offer.
Franchise Rollout: Standardization at Scale
Franchise operators face a unique challenge: build 20, 50, or 200 identical restaurants across different jurisdictions, different general contractors, and different construction labor markets, and deliver a consistent customer experience at every location. Conventional construction makes consistency expensive: each site requires a separate GC, separate subs, and separate quality control effort. Variation is inevitable, and the brand suffers when Location #47 doesn't look like Location #3.
Modular construction's factory platform solves franchise consistency at the manufacturing level:
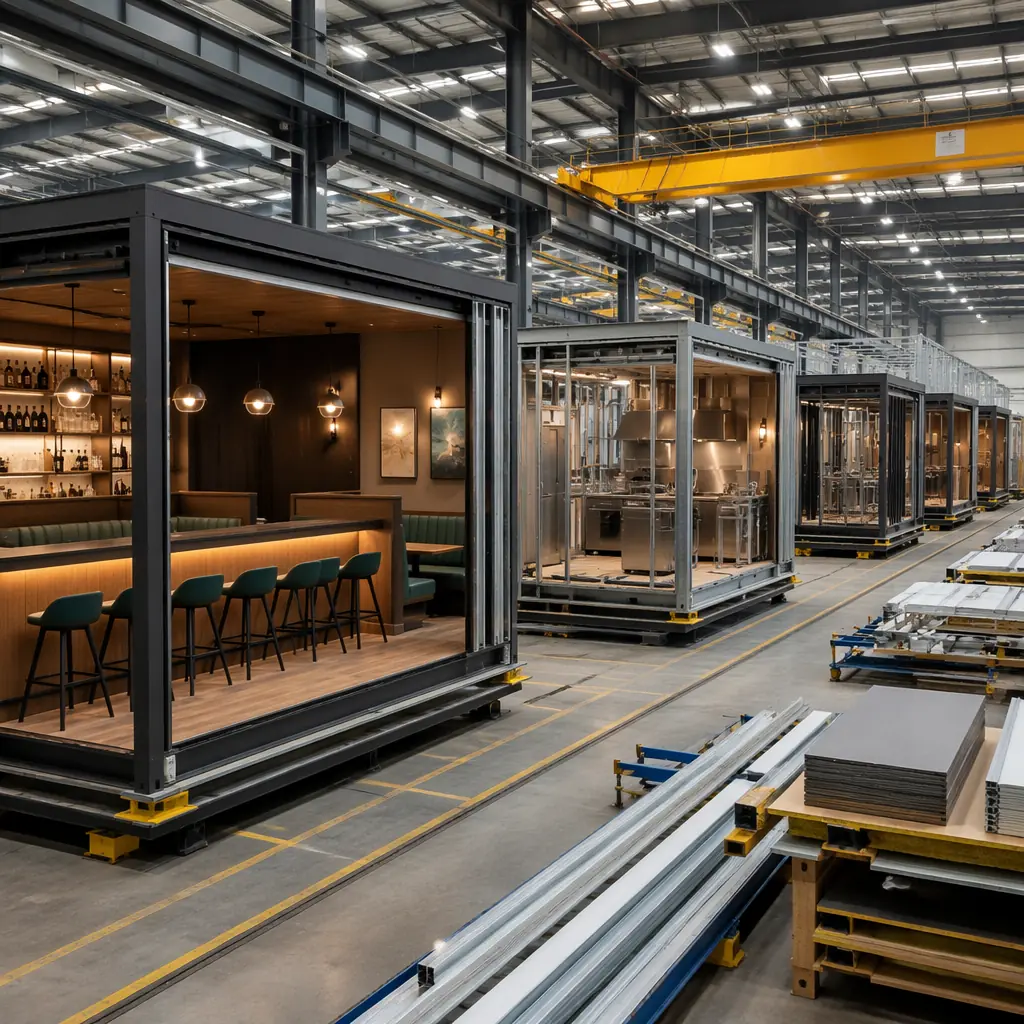
- Identical kitchen modules. A franchise operating 100 locations can order 100 identical kitchen modules from the same factory line, with the same MEP layout, the same equipment package, and the same finish specifications. The module that ships to Phoenix is the same module that ships to Portland, built by the same workforce using the same quality system.
- Local-content dining rooms. The back-of-house module is standardized; the front-of-house dining module can be customized for local market conditions (exterior cladding, signage integration, outdoor seating configuration) without affecting kitchen consistency. This split, standardized back-of-house + localized front-of-house, is the modular franchise model that maximizes both brand consistency and market fit.
- Predictable opening dates. When every restaurant takes 12–16 weeks from module order to turnover, franchise development teams can schedule openings with confidence. Marketing campaigns, staffing plans, and pre-opening training can be coordinated around a delivery date that doesn't slip because the factory schedule is inherently more predictable than site construction schedules subject to weather, labor availability, and trade coordination delays.
For operators building integrated commercial developments where restaurant modules are part of a larger project, our modular retail construction guide covers how restaurant, retail, and service tenants can be combined in a single modular platform.
Ventilation and Fire Suppression: The Kitchen-Specific Systems
Two systems define restaurant construction cost and complexity more than any others: the Type I grease hood and the associated fire suppression system. These systems are subject to NFPA 96 (ventilation control and fire protection of commercial cooking operations) and must be coordinated across mechanical, electrical, fire protection, and structural disciplines. A miscoordinated hood costs $15,000–$30,000 to rework and delays the project by 2–4 weeks.
MODURA's factory approach removes this coordination risk:
- Hood and ductwork. The Type I hood is mounted to the module ceiling structure in the factory, with welded 16-gauge black iron or 18-gauge stainless steel ductwork run through the module ceiling void to the roof penetration point. Fire wrap (2-hour rated enclosure per NFPA 96 §4.2) is factory-installed around the duct where it passes through the module structure.
- Fire suppression. The ANSUL R-102 or equivalent wet chemical fire suppression system is factory-installed with appliance-specific nozzles positioned per the UL 300 listing for each piece of cooking equipment. The system is piped to a factory-mounted control panel with manual pull station, gas valve interlock, and building fire alarm interface terminals.
- Makeup air. Factory-installed makeup air unit (typically 80% of exhaust volume) with heating coil for winter operation, ducted to deliver tempered air at the kitchen perimeter to avoid disrupting hood capture. The makeup air system is factory-balanced to maintain slight negative pressure in the kitchen relative to the dining room, preventing cooking odors from migrating to the customer area.
The cost impact of factory-installed hood systems is examined in our cost per square foot guide, which benchmarks restaurant-specific modular pricing against conventional construction across QSR, fast-casual, and full-service formats.
Cold Storage Integration
Restaurant refrigeration, walk-in coolers, freezers, and reach-in units, represents 15–20% of kitchen MEP cost and is a frequent source of construction defects (incorrect door swing, inadequate floor insulation, condensate drain routing errors). Modular construction integrates walk-in cooler panels as part of the kitchen module, with factory-installed refrigeration lines, condensate drains with proper slope, and door hardware adjusted and tested before shipment.
For restaurants requiring dedicated cold storage beyond standard kitchen refrigeration, commissary kitchens, central production kitchens, or distribution-focused operations, our cold storage modular facility guide covers temperature-controlled environments from -20°F freezer warehouses to 55°F produce storage.
Where the Restaurant Budget Actually Sits, Line by Line
The 40–50% schedule compression is not where the money differs. Some cost lines fall sharply under modular, one line rises, and one line that operators routinely assume is the supplier's is not. This is the breakdown we put in front of a franchise development team before a multi-unit tender, because every line below becomes a contract boundary:
| Cost Line | Share of Build Budget | Who Carries It | How Modular Changes It |
|---|---|---|---|
| Kitchen module (shell, MEP rough-in, finishes) | 34–42% | MODURA | Higher unit price than a stick-built shell, but it ships with plumbing stub-outs labelled, electrical panels pre-wired and hood ductwork already run, so the on-site MEP rough-in phase largely disappears |
| Type I hood, ductwork & UL 300 suppression | 7–11% | MODURA | Factory-mounted and fire-wrapped to the roof penetration. This is the single line that most often blows a conventional budget, because a miscoordinated hood costs $15,000–$30,000 to rework and 2–4 weeks of schedule. Details in our fire safety construction guide |
| Walk-in coolers, freezers & refrigeration lines | 8–13% | MODURA | Door swing, floor insulation and condensate slope are set and tested in the factory. These three defects are the most common restaurant punch-list items and the hardest to correct after the floor is poured. See cold storage construction |
| Freight to site & crane set | 4–8% | Usually client | The one line where modular costs more. A 3–5 module restaurant typically cranes in over 2–3 days, so the premium is small in absolute terms but it is real and it scales with distance from the nearest factory |
| Foundation pad, utilities to the pad, grease interceptor | 9–15% | Client (site package) | Point-load pads replace continuous footings, but they must be level to tolerance and poured before the crane arrives. Utilities, grease interceptor and connection points remain site scope. Tolerances are in foundation systems |
| Health department plan review & local permits | 1–3% | Client | Largely unchanged in cost, but sharply reduced in duration: factory-built kitchens cut the revision cycles that add 2–3 weeks each. The pre-approved submittal path is covered in permitting & zoning |
| Lease carry & management overhead during construction | $25,000–$40,000 / month | Client | Not a construction line at all, and usually the largest number on the page. Every month removed from the programme removes this cost in full, which is why a 6-month delay on a $1.2M build-out burns $180,000 before the first cover is served |
The honest read: modular does not make a restaurant cheap. It makes it early, and on a leased site early is the only number that compounds. Roughly two-thirds of the budget moves into a factory where it is produced at a fixed rate with a stable labour pool, while the on-site share, freight excepted, compresses into a short crane-and-connect window that is far easier to hold to a date.
Franchise Rollout Programme, Site Selection to Opening Day
The 12–16 week figure is a range, and where a unit lands inside it is decided by how early the pad and permit gates close, not by factory capacity. This is the milestone sequence we hold a franchise rollout to, with the conventional comparator beside it:
| Milestone | Modular | Conventional | What Gates It |
|---|---|---|---|
| Prototype design freeze | Month 0–1 | Month 0–2 | Kitchen equipment package and hood layout must be locked before module fabrication starts; changing the equipment list afterwards is the most expensive change a franchise can make |
| Health department & building plan review | Month 1–2.5 | Month 1–4 | Factory-standard NSF details cut the revision cycles. Some jurisdictions offer pre-approved modular submittal programmes for repeat prototypes |
| Site pad, utilities & grease interceptor | Month 2–3.5 | Month 2–6 | Pad must be level to tolerance and poured before the crane date. This gate, not the factory, is what usually moves a modular opening |
| Module fabrication in factory | Month 1.5–3.5 | n/a (site framing) | Runs concurrently with site works, which is the whole schedule gain. Weather does not enter the critical path |
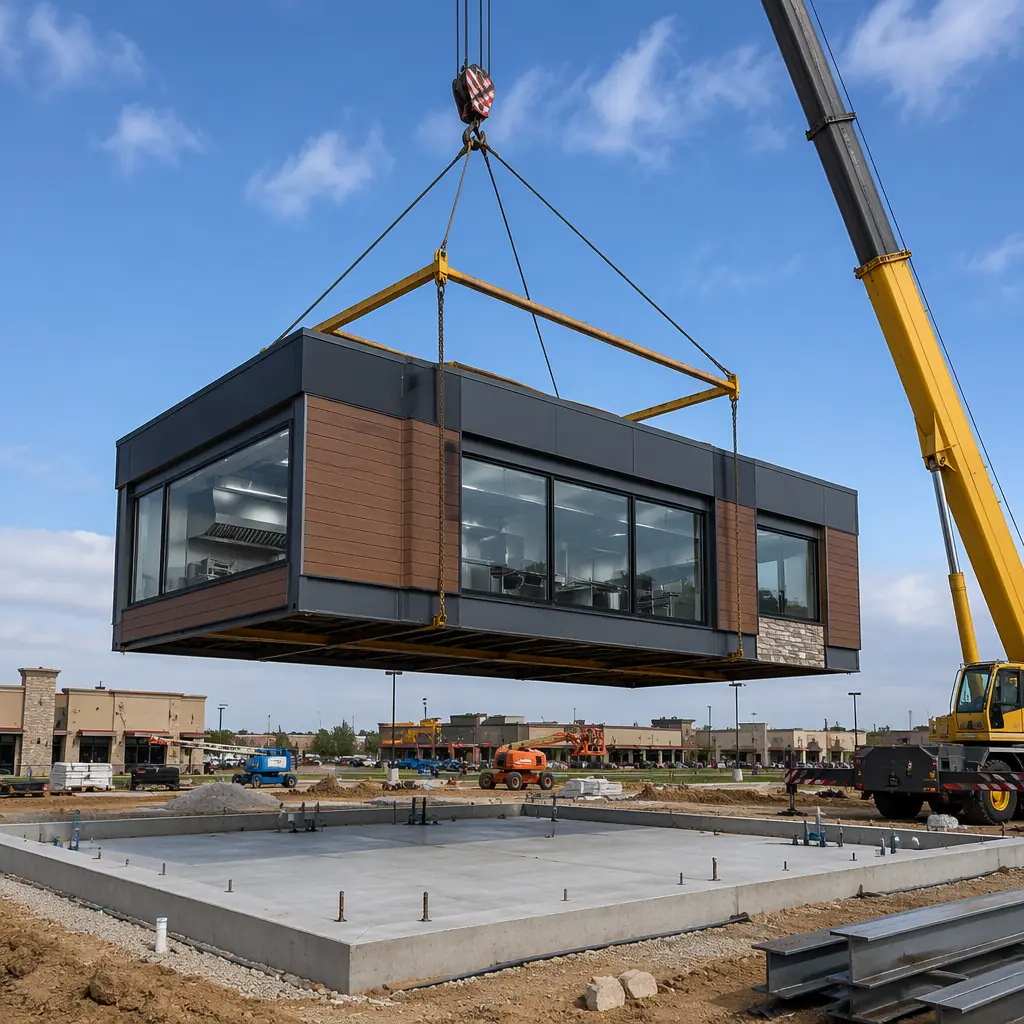
| Delivery, crane set & module connections | Month 3.5–4.5 | Month 6–8 | A single restaurant cranes in over 2–3 days; inter-module MEP joints are closed per the interface schedule in MEP systems integration |
| Final connections, commissioning & health sign-off | Month 4.5–5.5 | Month 8–11 | Gas interlock, hood commissioning, fire suppression test and health inspection. Equipment is already tested in the factory, so this phase is connection and verification rather than discovery |
| Opening day | Month 5.5–6 | Month 10–13 | A 4–7 month earlier opening per unit, which for a 20-unit programme is the difference between one rollout year and two |
The Developer's Case: Restaurant Pads in Mixed-Use Projects
Mixed-use developers increasingly include restaurant pads as ground-floor anchors that drive foot traffic and increase residential and office lease values. But restaurant build-out is the longest-lead item in a mixed-use project, and a delayed restaurant opening means the entire development launches without its anchor tenant. Modular restaurant modules solve this by decoupling the restaurant build-out from the core-and-shell construction schedule: the restaurant module is fabricated concurrently with the building structure and craned into the ground-floor pad when the building envelope is complete, reducing the restaurant critical path from 6–8 months to 8–12 weeks. For turnkey project delivery, see our turnkey modular construction overview.
How Many Units Can a Franchise Roll Out Concurrently?
The concurrency limit is not a factory constraint. It is set by how many site pads, health jurisdictions and local installation crews a franchise development team can genuinely run at once. This is what each rollout pace physically requires, and the point at which it stops being a construction question and becomes a development-capacity question:
| Rollout Pace | What the Client Gets | What It Physically Requires | Implication |
|---|---|---|---|
| 1–3 units / year | Single prototype, standard module | 1 site pad open at a time; 1 local crane mob; 1 health jurisdiction | No concurrency constraint. This is the pace where modular's advantage is almost entirely schedule, not scale |
| 4–10 units / year | Repeat prototype, localised front-of-house finishes | 2–3 pads open concurrently; 2 crane mobs; 3–5 jurisdictions; a standing install crew | First pace where factory standardisation produces visible cost benefit, because the prototype is amortised across units |
| 11–25 units / year | Same kitchen module across all regions, different dining format | 4–6 pads concurrent; regional crane contracts; dedicated rollout PM; per-state permit tracking | Requires a named rollout programme manager. The bottleneck becomes permit administration, not construction |
| 25+ units / year | Multi-format, multi-region, dedicated production slots | Reserved factory slots per quarter; 8+ pads concurrent; standing crane and install contracts; regional jurisdiction map | Must reserve factory capacity in advance. At this pace the constraint is production slots and pad readiness, and both are booked a quarter out |
Questions We Are Asked Before Every Restaurant Contract
These are the objections that recur in nearly every restaurant construction enquiry, whether it is a single operator or a 50-unit franchise. We answer them in writing rather than verbally, because each one becomes a contract term:
- “What is the minimum number of units where modular actually pays?” A single restaurant can still win on schedule alone if the site is leased and carrying cost is high, but the cost advantage really begins at the second and third unit, where the prototype is amortised. Below three units we are selling speed, not price, and we say so. The current per-square-foot ranges are in our cost per square foot guide.
- “What happens if the site pad is not ready when the modules arrive?” Modules can be held in factory storage for a defined period at a stated daily rate, but this is a cost, not a neutral delay, and it is the most common way a modular schedule advantage is given away. It is why the pad gate is on the critical path in the programme table above. Pad tolerances are set out in our foundation systems guide.
- “Can the kitchen module be changed after the prototype is locked?” Yes, but changes after fabrication starts are the most expensive changes a franchise can make, because hood, suppression and refrigeration are built into the module structure. We ask for the equipment package to be frozen before the first module is cut and for any later change to be priced as a variation. How that split is documented is covered in warranties & structural guarantees.
- “Is a modular kitchen really treated the same as a site-built one by the health department?” The Food Code applies to the kitchen, not to how it was assembled, and factory-standard NSF details typically clear review faster because floor slope, coved base and hand sink distances are already resolved in the design. What is not simplified is local adoption of the code, which varies by jurisdiction. The interaction is covered in permitting & zoning.
- “What about a dark kitchen or delivery-only format?” Ghost kitchens are the cleanest fit for modular because they are kitchen and dispatch only, with no dining-room finish or customer-facing front of house to localise. The venue type is covered in ghost kitchen & commissary facilities, and the mixed-tenant case in modular retail construction.
- “What documentation do we get for lender due diligence?” Every module carries a digital record: material certifications, weld and pressure-test evidence, hood and suppression commissioning records. That produces an audit trail site construction cannot match, which matters when a rollout is financed against opening milestones. The economics are in our developer ROI guide.
MODURA has delivered commercial modules for restaurant, retail and food-service operators across multiple markets, supported by certified manufacturing partners and a production model that runs kitchen fabrication concurrently with site works. For operators scaling a proven concept, modular is no longer an interesting alternative to conventional build-out. It is increasingly the baseline against which conventional bids are measured.