The AI infrastructure build-out is the largest capital deployment in data center history. McKinsey estimates $1.8 trillion will flow into AI data center construction globally between 2025 and 2030, a market growing at 23% CAGR. NVIDIA shipped 3.8 million H100-equivalent GPUs in 2025 alone, and each rack of H100s draws 40-50kW, roughly 5-8x the power density of a traditional enterprise server rack. Traditional data center construction cannot keep pace: a ground-up 50MW AI data center takes 24-30 months from site selection to commissioning using conventional methods. Modular prefabricated construction cuts this to 12-16 months, a 40-50% reduction, while delivering the precision mechanical and electrical infrastructure that GPU clusters demand.
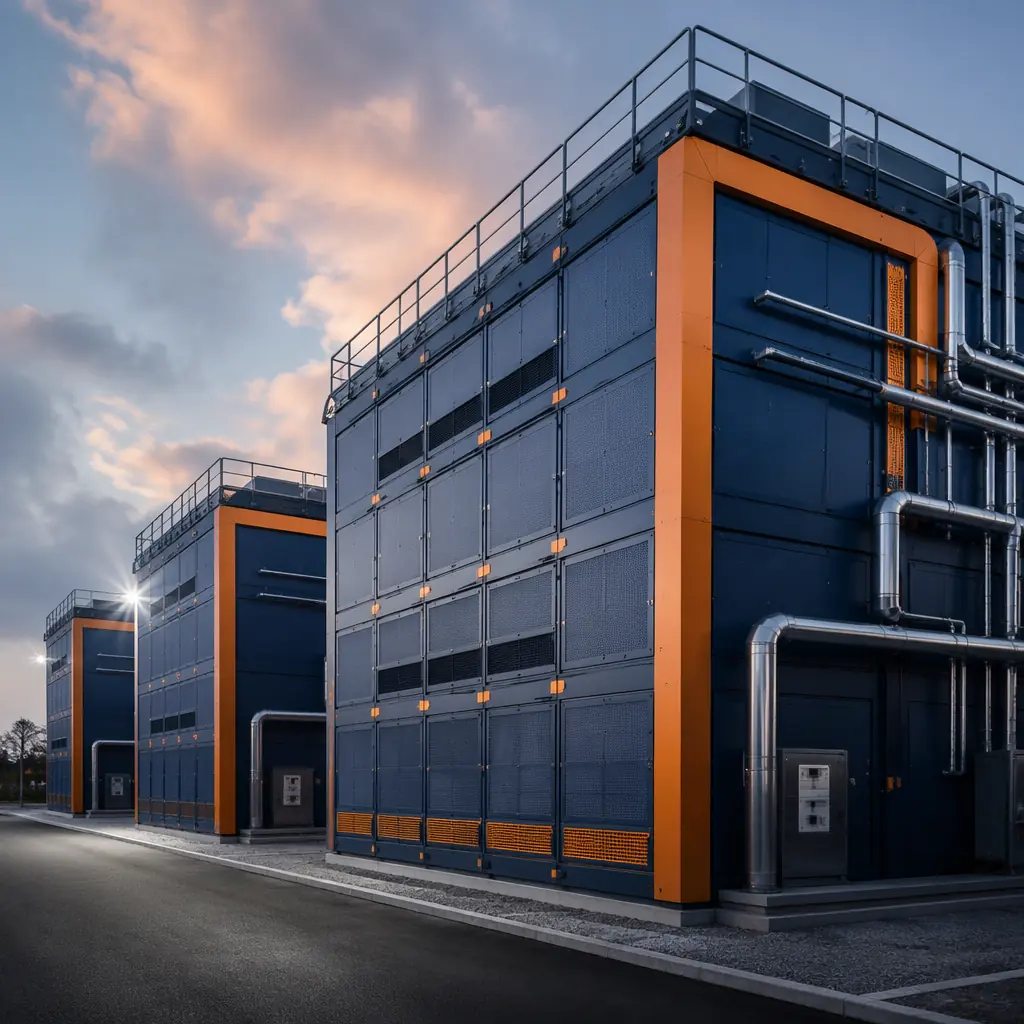
Why AI Compute Breaks Traditional Data Center Construction
AI training and inference workloads impose three requirements that conventional data center design struggles to meet simultaneously:
- Power density of 50-100kW per rack: An NVIDIA GB200 NVL72 rack consumes approximately 120kW, equivalent to 15-20 traditional server racks in a single cabinet footprint. Supporting this density requires busway distribution at 415V/480V, not legacy 208V PDUs, and the switchgear lead time alone for a 50MW AI campus is currently 52-78 weeks. Modular data center construction addresses this by integrating medium-voltage switchgear, transformers, and busway distribution into factory-built power modules that are manufactured in parallel with site preparation, eliminating the 12-18 month electrical equipment queue from the critical path.
- Direct-to-chip liquid cooling: Air cooling hits its practical limit at 25-30kW per rack. Above 40kW, direct-to-chip liquid cooling or immersion cooling becomes mandatory. This requires a facility-wide secondary cooling loop with CDU (coolant distribution units) on every data hall floor, plus rooftop dry coolers or cooling towers sized for 100% of IT load. For a 10MW AI data hall, that's approximately 2,850 tons of heat rejection. 3-4x what a traditional enterprise data hall of the same square footage requires. Modular factory-built data halls pre-integrate CDU racks, piping headers, and leak detection systems before the module leaves the factory, eliminating the 8-10 weeks of on-site MEP coordination that liquid cooling retrofits demand in traditional builds.
- Network fabric density: AI training clusters use 400Gb/s and 800Gb/s InfiniBand or RoCE fabrics with 1:1 non-blocking topologies. A 1,000-GPU cluster requires approximately 2,000 transceivers and 3-5km of fiber patch cables, all of which must be installed, tested, and certified before the first training job runs. In a traditional build, network cabling happens after the data hall is enclosed, week 18-20 in a 24-week schedule. In a modular build, the network fabric is pre-cabled, pre-tested, and pre-certified at the factory, shrinking the on-site network commissioning window from 6 weeks to 2 weeks.
These aren't incremental differences. Uptime Institute's 2025 survey found that 58% of AI data center projects experienced schedule delays exceeding 12 weeks, with the top three causes being: electrical equipment lead times (cited by 72% of operators), liquid cooling integration complexity (64%), and skilled labor shortages for high-density MEP installation (58%). As we've shown in our analysis of modular data center construction, factory-controlled production systematically eliminates all three of these delay vectors. Our BIM-to-factory digital workflow ensures the electrical, mechanical, and network systems are installed to ±2mm precision, the tolerance level that AI infrastructure demands.
Modular AI Data Center Architecture
A modular AI data center isn't a single factory-built box, it's an assembly of purpose-built modules, each optimized for a specific infrastructure function, connected on site to form a complete facility.
Data Hall Modules
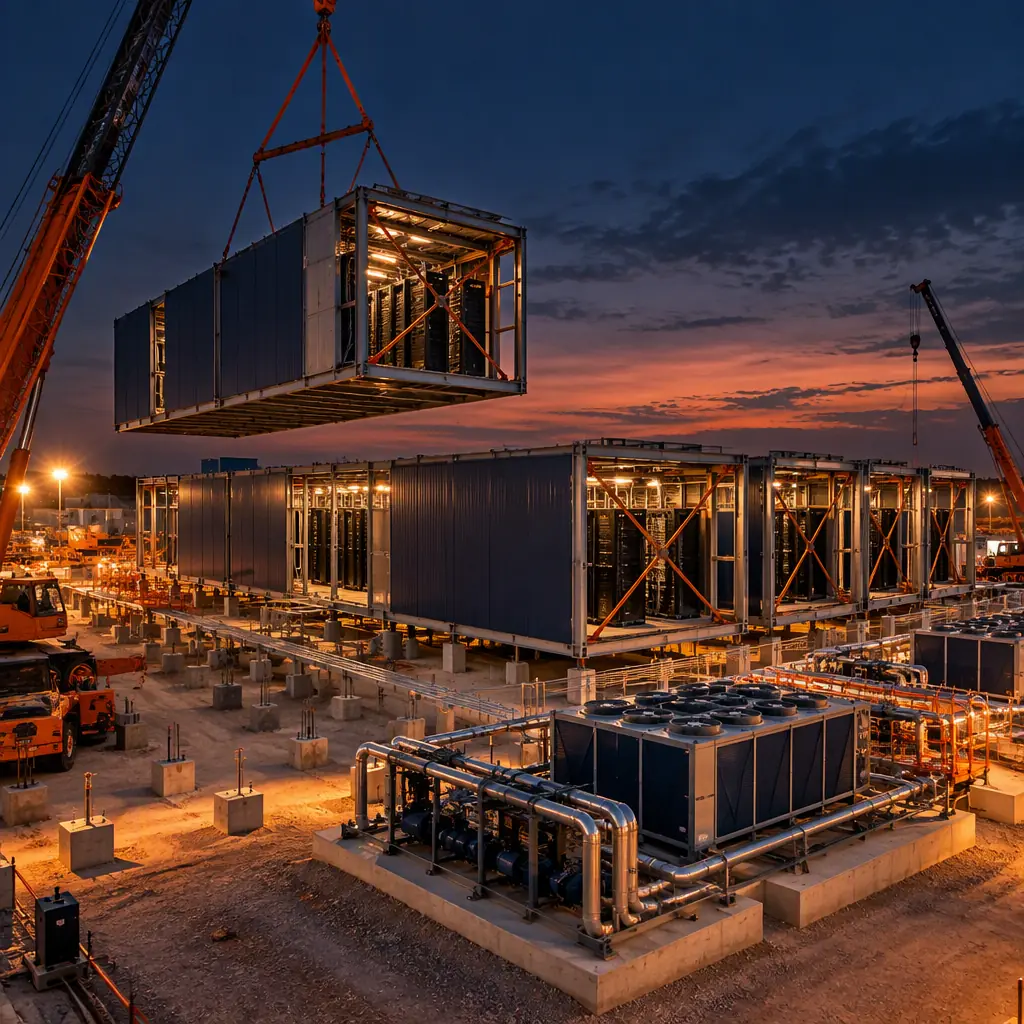
The core unit: a 14' × 60' steel-frame module (840 sq ft) housing 8-12 racks per module. Each data hall module arrives with: cold-aisle containment structure pre-installed, overhead busway pre-mounted, direct-to-chip liquid cooling CDU rack pre-integrated, primary and secondary piping headers pre-routed and pressure-tested, fiber patch panels pre-terminated, and the raised floor system (24" clear height for under-floor cooling distribution) installed at the factory. Twelve data hall modules connected side-by-side create a 10,000 sq ft GPU cluster floor supporting approximately 120 racks at 50kW average density, 6MW of IT load in a single deployment unit.
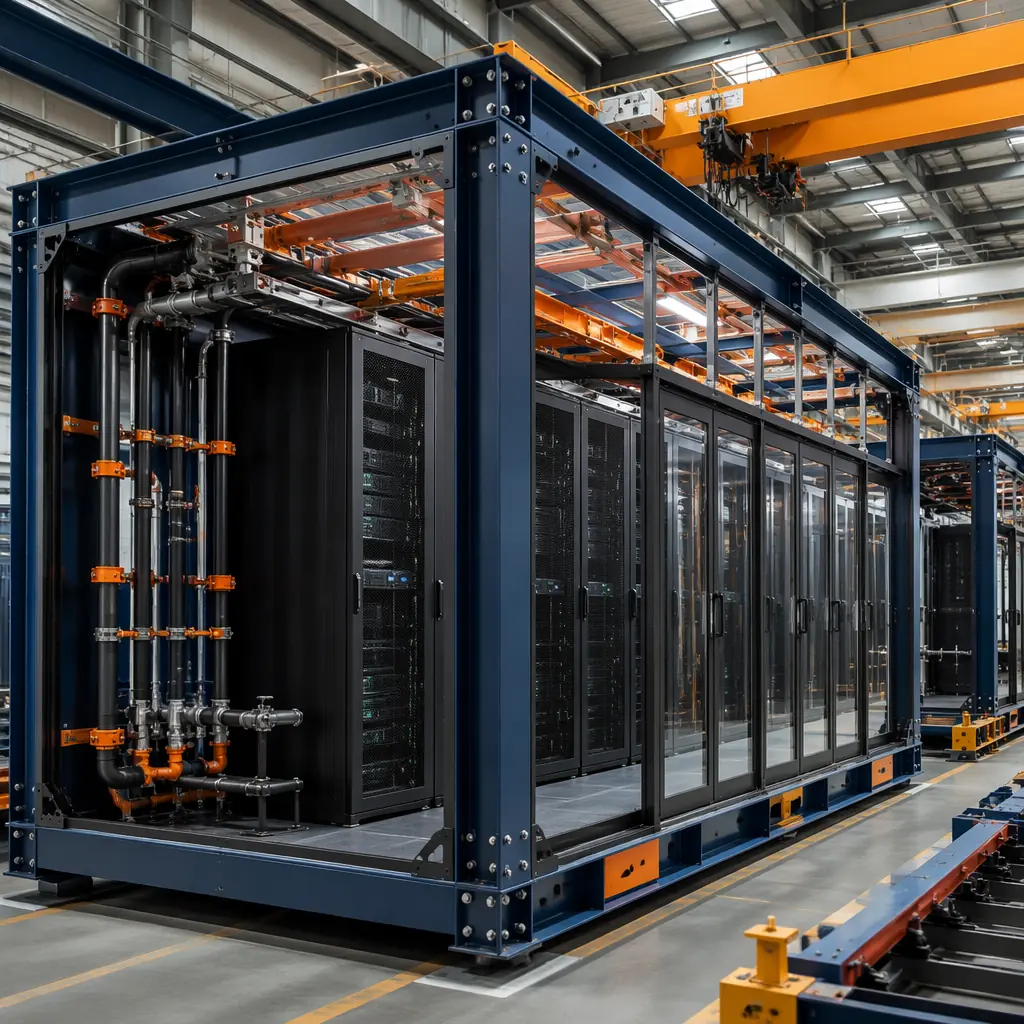
Power Infrastructure Modules
AI workloads demand power infrastructure that traditional construction methods simply cannot procure fast enough. Modular power skids, factory-built in 40' ISO container footprints, integrate medium-voltage switchgear, dry-type transformers (415V to 480V step-down), UPS systems with 5-minute flywheel or 10-minute battery backup, and main distribution panels. A single power module supports 2-3MW of IT load; a 50MW AI campus requires 18-20 power modules. Critically, these modules are manufactured in 16-20 weeks in parallel with site civil work, compared to the 52-78 week lead time for site-assembled medium-voltage switchgear. The result: electrical infrastructure is no longer the longest-lead item on an AI data center construction program.
Cooling Plant Modules
For liquid-cooled AI clusters, the cooling plant is often the most spatially intensive subsystem. A 10MW data hall with direct-to-chip cooling requires approximately 1,400 GPM of treated process water circulating through CDUs, dry coolers, and storage tanks. Modular cooling plants, built as interconnected skid-mounted modules housing pumps, plate-and-frame heat exchangers, filtration systems, chemical treatment dosing units, and controls, reduce on-site cooling plant construction from 14-16 weeks to 4-6 weeks of module interconnection. As we documented in our guide to modular MEP systems integration, pre-integrated mechanical modules achieve 95%+ first-pass commissioning rates compared to 60-70% for field-assembled systems.
Speed-to-Market: The Economic Case for Modular AI Infrastructure
The business case for modular AI data center construction isn't about saving construction cost per square foot, it's about time-to-revenue. An AI data center generating $50 million in annual colocation revenue loses approximately $4.2 million for every month of delayed commissioning. When the alternative is a 30-month traditional build versus a 14-month modular build, the 16-month acceleration represents $67 million in recovered revenue potential, far exceeding any marginal construction cost difference.
| Project Phase | Traditional Build (50MW) | Modular Build (50MW) |
|---|---|---|
| Site selection & permitting | 4-6 months | 4-6 months (identical) |
| Civil & foundation work | 5-7 months | 4-5 months (reduced scope) |
| Building enclosure | 6-8 months | Concurrent with factory production |
| MEP rough-in & electrical | 8-10 months (after enclosure) | Pre-integrated in factory modules |
| Commissioning & acceptance | 3-4 months | 1-2 months (pre-tested at factory) |
| Total: Site selection to live load | 26-35 months | 12-16 months |
For colocation providers executing multi-site AI infrastructure rollouts, the program-level acceleration compounds. As we've analyzed in our comparison of modular data center TCO: build vs buy, modular construction's schedule certainty is worth 8-12% in effective IRR improvement for multi-facility programs. Developers scaling from one facility to five can reliably forecast commissioning dates 12 months out, something traditional construction's 58% delay rate makes impossible. MODURA's modular foundation systems further compress site preparation timelines, particularly on the greenfield sites that AI data center developers increasingly target for lower energy costs.
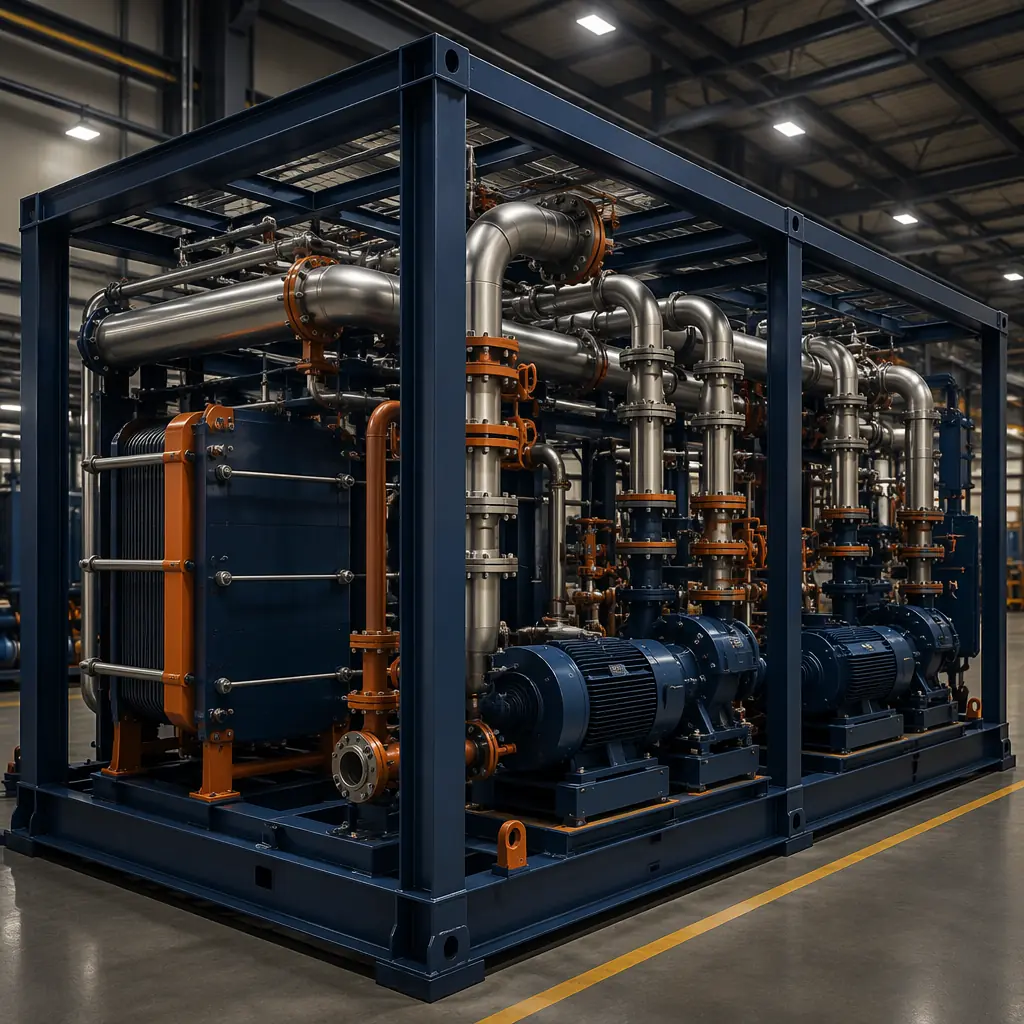
Designing for GPU Density: Structural and Thermal Considerations
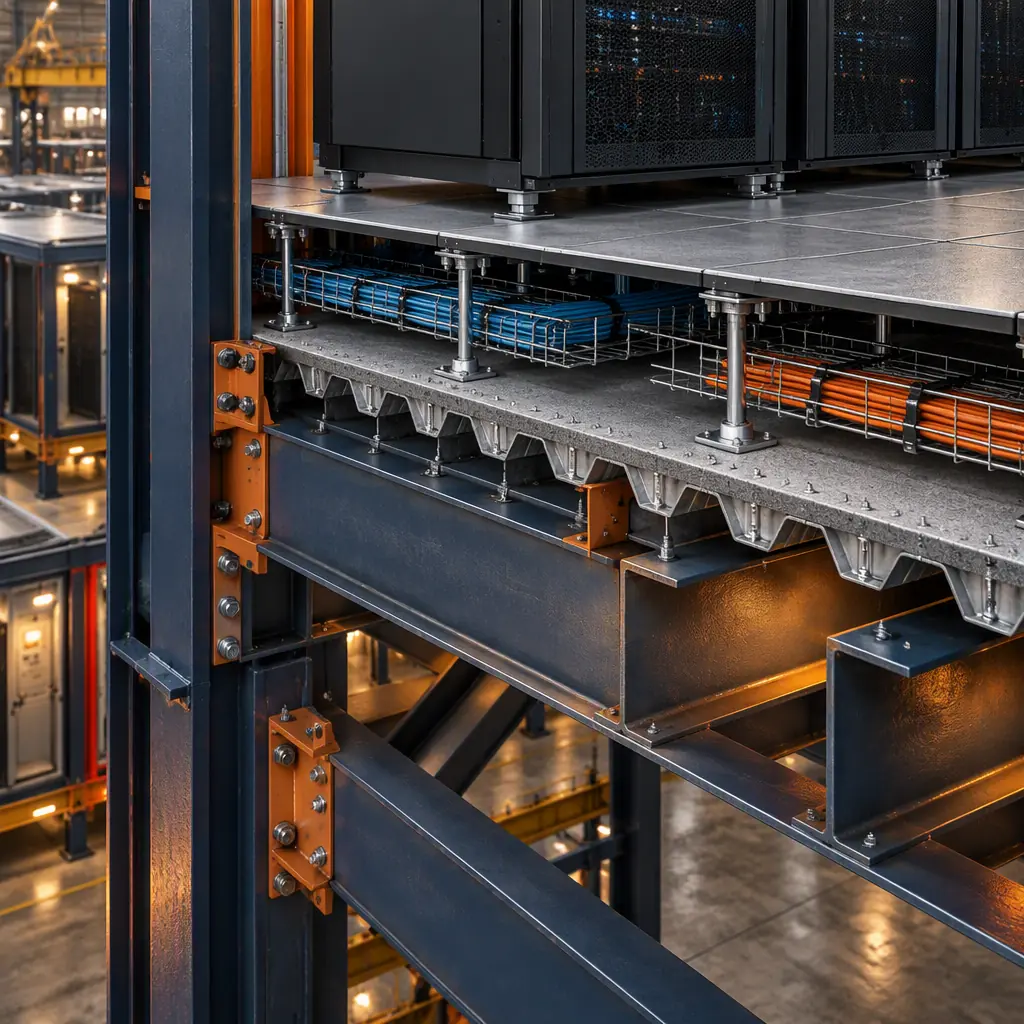
AI data centers impose floor loading requirements that exceed traditional data center designs. An NVIDIA DGX GB200 rack with liquid cooling infrastructure weighs approximately 2,500 kg (5,500 lbs), roughly 3x a standard enterprise server rack. Across a 120-rack data hall, that's 300 metric tons of concentrated IT load, requiring floor slab designs of 150-200 psf (compared to 100-125 psf for enterprise data halls). Modular construction's steel frame inherently handles these loads: MODURA's standard data hall module is engineered for 250 psf live load, with structural capacity pre-verified in the factory rather than relying on field-poured concrete slab inspections.
The acoustic environment also demands attention. AI GPU clusters operating at full TDP produce 85-90 dBA of fan noise, comparable to a manufacturing floor. While operators rarely occupy the data hall during production runs, adjacent office and NOC spaces require STC 55+ separation. Factory-built modules achieve this through pre-installed acoustic insulation in wall and ceiling cavities, tested at the factory before module shipment. For developers evaluating noise-sensitive AI deployments adjacent to residential or commercial zones, our guide to modular building acoustics and soundproofing details STC ratings achievable with different wall assembly configurations.
Scalability: From Edge Inference to Hyperscale Training
Modular AI data center construction scales across the full spectrum of AI infrastructure:
- Edge inference nodes (100-500kW, 4-8 racks): 1-2 data hall modules deployed at telecom aggregation points or enterprise campuses. Pre-integrated with 20kW/rack cooling and local UPS. Deployment time: 8-10 weeks from order to live load. Use case: low-latency inference for autonomous systems, real-time video analytics, and on-premises LLM serving.
- Regional training clusters (2-10MW, 40-200 racks): 4-12 data hall modules with dedicated power and cooling modules. Deployment time: 6-9 months. Use case: enterprise fine-tuning clusters, regional cloud AI zones, pharmaceutical molecular dynamics simulation.
- Hyperscale training campuses (50-200MW, 1,000-4,000 racks): 18-70 data hall modules, 6-25 power modules, site-built central cooling plant. Deployment time: 12-16 months for first 50MW phase. Use case: foundation model training, national AI research infrastructure, sovereign AI cloud deployments.
This modular scalability is what makes prefabricated construction the default choice for AI infrastructure programs. A developer can commission a 500kW edge node in Q1, add 5MW of training capacity in Q3, and scale to 50MW by Q4 of the following year, all using the same factory-built module platform, the same supply chain, and the same installation methodology. Compare this to the traditional approach: three entirely separate design-bid-build projects, three separate GC teams, and zero cross-project learning. For developers executing geographic expansion strategies, deploying AI infrastructure across multiple countries simultaneously, our cross-border modular logistics guide covers customs, compliance, and multi-country module shipping.
Getting Started: Feasibility Assessment for AI Infrastructure
MODURA's approach to AI data center construction begins with a 3-week feasibility assessment covering: power availability analysis at candidate sites (transmission-level grid interconnection, not just distribution-level), cooling water source evaluation (municipal, well, or closed-loop options), module configuration for target GPU density (H100, H200, B200, or GB200 clusters), and a phased deployment schedule with milestone dates. The assessment includes a preliminary total cost of ownership model comparing modular to traditional construction, with sensitivity analysis for power cost escalation (+15% to +40% scenarios based on regional grid forecasts) and GPU technology refresh cycles (24-month vs 36-month).
Structural and Environmental Design Loads for AI Halls
The loads in an AI data hall are not the loads in an office building, and they are not the loads in a conventional enterprise data center either. GPU cabinets are both heavier and far more thermally aggressive than the racks the modular industry spent the last decade designing for. The table below states the design values MODURA builds to, the standard or method each value is verified against, and why getting that specific number wrong is expensive later.
| Design Parameter | Value MODURA Builds To | Verified By | What It Protects |
|---|---|---|---|
| Live floor load, GPU rows | 1,500 to 2,500 kg/m² (300 to 500 psf) | Structural calculation per ASCE 7 load combinations, third-party stamped | Prevents mid-project floor reinforcement. A 500 kg/m² under-design discovered after modules are cast cannot be fixed in the factory. |
| Point load at cabinet feet | 900 kg per foot minimum, 1,200 kg where B200-class racks are confirmed | Foot-pad bearing calculation, checked against rack vendor cut sheet | Protects the raised-floor grid. Crushed pedestals under a loaded row mean emptying the row to repair it. |
| Floor flatness / levelness | FF 50 / FL 35 minimum across each module | F-number survey at the factory, report shipped with the module | Rack alignment and rack-to-rack busbar gaps. Site-poured slabs routinely miss this and the fix is grinding. |
| Thermal load density | 30 to 60 kW per rack, up to 130 kW for GB200 NVL72 rows | Heat balance per module, HVAC selection at the higher figure | Prevents cooling shortfall at commissioning. Designing to the average rather than the peak is the single most common AI hall error. |
| Structural natural frequency | 3 Hz to 8 Hz, avoiding 20 Hz to 30 Hz | Modal analysis per module type | Protects against floor-borne vibration affecting high-speed interconnect and spinning media. Avoids resonance with cooling plant rotation. |
| Air change rate, hot aisle | 8 to 12 ACH with containment, 20+ ACH for high-density rows | CFD model delivered with the design package | Prevents inlet temperature drift above ASHRAE A1 envelope, which triggers GPU thermal throttling before any alarm sounds. |
| Acoustic limit, occupied spaces | NC-40 maximum, NC-35 where staff work continuously | Factory acoustic test on the plant module | Protects operator health and compliance. Liquid-cooling pump and CDU noise is not covered by general office NC assumptions (which sit at NC-30). |
The last column is where most modular programmes lose money. A design load is only useful if somebody can point at the evidence that confirms it, so every figure above ships with a stamped calculation, a survey report, or a CFD model, not a specification sheet quote. Buyers comparing modular data center proposals should ask for these documents by name before comparing price, because the cheapest bid is very often the one that quietly designed its floor to 300 psf. Our modular construction cost per square foot breakdown explains where the extra structural steel sits in the cost line, and how to tell a realistic bid from a thin one.
The AI Data Center Interface: Who Owns What
Modular AI halls fail in a predictable place. The factory scope is well defined and the client scope is well defined, but the seam between them is not, and that seam is where variation orders are born. The matrix below names each interface explicitly, and it carries a fourth column stating the decision that removes the ambiguity before the contract is signed rather than after the first module ships.
| Interface | MODURA Scope | Client / OEM Scope | Decision That Closes It |
|---|---|---|---|
| Substructure and foundations | Schematic pier grid, load table, anchor layout, tolerance envelope | Site survey, geotechnical report, local foundation design and construction | Who signs the setting-out tolerance, and what happens if the actual piers fall outside it |
| Power from utility to hall | Module-level switchgear, busway within the module up to the demarcation point | Utility interconnection, MV distribution, transformers, upstream protection study | The physical demarcation point, named on the single-line diagram, signed by both parties |
| UPS and battery systems | Module structural provisions, load-bearing pads, ventilation routes, fire compartment | UPS and battery selection, wiring, protection settings, commissioning | Whether battery thermal runaway venting is a factory provision or a site addition, decided before the fire strategy is submitted |
| Cooling plant and CDUs | Mounting, vibration isolation, hydraulic connections to the module boundary, factory acoustic test | Chiller and CDU supply, primary/secondary loop design, water treatment, commissioning | Flow rate, supply temperature and pressure at the module boundary, fixed as scheduled values not as achievable ranges |
| Liquid cooling manifolds and drip protection | Floor drainage, containment, drip trays, leak-detection zones cast into the module | Manifold supply, CDU-to-manifold pipework, fluid specification, leak sensor integration | Test pressure at the factory hydraulic test and the acceptance criteria for a passed test |
| IT and network cabling | Pathways, containment, cable entry positions, separation from power routes | Cable supply, termination, labelling, testing, commissioning | Whether structured cabling is terminated factory-side or delivered as unterminated pathway only |
| Fire detection and suppression | Detection zoning in the module, suppression pipework provisions, penetration sealing, witnesses for factory FAT | Agent supply, panel configuration and programming, final site commissioning | Which authority has jurisdiction, and whether the factory test satisfies it or requires a repeat at site |
| Commissioning and handover | Factory acceptance test per module, integrated systems test at the factory where modules are pre-assembled | Site integrated systems test, load bank testing, operator training, witness sign-off | What exactly the factory FAT covers and what evidence the client accepts in place of a site re-test |
There is a straightforward test for whether an interface is genuinely closed: ask who pays if it is discovered to be wrong on site. If the answer takes more than one sentence, the interface is still open. Buyers can use this matrix as a checklist against any modular data center bid, and our colocation build-to-suit guide walks through the same scope logic from the operator side, covering where landlord-scope ends and tenant-scope begins in a leased facility. For conventional industrial projects with the same boundary problem, see heavy industrial modular construction.
What Actually Moves the Cost of a Modular AI Facility
A single price per MW is not a useful planning number for AI infrastructure, because two buildings with the same nominal IT capacity can differ by more than it costs to build the shell. The drivers below are listed in the order they typically dominate a budget, with indicative low and high figures and the specific decision that shifts a project within that range.
| Cost Driver | Low End | High End | What Moves It |
|---|---|---|---|
| Structural steel for GPU floor loading | USD 55/m² of floor | USD 130/m² of floor | Design floor load. Moving from 300 psf to 500 psf typically adds roughly 60 to 80 percent to the frame cost of the affected bays, and it is almost free to decide at design stage and very expensive to retrofit. |
| Cooling architecture | USD 380/kW | USD 690/kW | Air, rear-door heat exchanger, or direct-to-chip liquid. Liquid cooling raises capex but lifts achievable density and cuts fan power; the crossover is usually material above about 25 kW per rack. |
| Power distribution and redundancy | USD 420/kW | USD 1,150/kW | N, N+1 or 2N. Each step up in topology roughly multiplies the switchgear and UPS line rather than adding a percentage to it, which is why redundancy is a specification decision, not an upgrade. |
| Distance from factory to site | USD 60/tonne | USD 210/tonne | Road, rail and sea leg, plus module width against local permit limits. Wide-load escort requirements in the final 200 km frequently exceed the cost of the long-haul leg, so the last mile deserves its own quote. |
| Programme compression | 0 percent premium | 12 to 18 percent premium | Whether modules are ordered against a frozen design or reworked during production. Change control after fixture release is what turns a fast programme into an expensive one; the fast programme itself costs nothing extra. |
| Site works and enabling | USD 8/m² of site | USD 45/m² of site | Greenfield versus constrained urban infill. Access road capacity, crane pad, laydown area and temporary power are all site-side and none of them travel with the module. |
Worked example for a 20 MW facility, expressed per MW so it scales to other programme sizes. A conventional 2N air-cooled design lands near USD 6.4M per MW before site works and module transport. Dropping to N+1 topology and moving to liquid cooling at 45 kW per rack typically brings the same IT capacity to approximately USD 4.1M per MW, while raising rack density enough that some halls in the layout consolidate entirely. Structural allowances and site works do not disappear, which is why the saving is roughly a third rather than the half that headline comparisons sometimes imply. Our total cost planning guide covers the same arithmetic over a full asset life, and data center TCO: build versus buy compares modular capex against leased colocation capacity, which is the comparison most enterprise buyers are actually running.
Verifying a Modular AI Data Center Supplier
Most of what separates a credible modular AI data center supplier from one that is assembling steel boxes with a data center label can be established without leaving a desk. Each of the checks below can be completed from documents, and each one is a question a supplier with real AI hall experience can answer immediately.
- Ask for the stamped structural calculation, not the load figure. A supplier who quotes 500 psf without producing a third-party calculation has either designed it or copied it from a brochure, and the two are indistinguishable until it is too late.
- Match the certification holder to the factory address. An ISO 9001 certificate issued to a head office or a trading entity does not cover the production line. Check the address on the certificate against the address where your modules will actually be welded.
- Ask what the factory acceptance test covers. For a data hall module the useful answers are hydraulic test pressure, insulation resistance readings, containment leak test and a witnessed detection zone walk. A FAT that only covers visual inspection is a shipping check, not a quality gate.
- Ask for a completed project with the same density class. Not the same capacity, the same density. A 5 MW facility at 8 kW per rack and a 5 MW facility at 45 kW per rack are different engineering problems, and experience in the first does not transfer to the second.
- Ask who writes the integrated systems test script. If the answer is "we will provide one after delivery," the commissioning risk sits with the client. It should be a named deliverable in the contract scope.
- Ask for the transport route survey. Not the transport quote, the route survey, covering permits, clearances and the final-mile constraints. Hidden route restrictions are among the most common causes of a late module arrival.
- Ask what the tolerance envelope is and who owns a breach of it. Factory-built modules arrive accurate; the foundations they land on frequently do not. The contract should state the envelope, the measurement method and the remedy.
Two of these checks matter more than the rest. The stamped calculation and the route survey are the two places where optimism in a proposal turns into cost for the buyer, and both are cheap to verify in advance. Our RFP and procurement guide covers how to write these requirements into the tender document itself rather than negotiating them afterwards, and bid comparison for modular construction shows how to normalise quotes that appear comparable but carry different scope.
Questions We Are Asked Before Every AI Data Center Contract
Can a modular hall really support 130 kW racks?
Yes, and the constraint is rarely the structure. At 130 kW per rack the design is driven by liquid cooling distribution, floor drainage and leak detection rather than by steel. We build the module with the manifolds, drip trays and drainage cast in, and the CDU selection stays with the client because it usually follows their existing fleet standard.
What happens if the site foundations are out of tolerance?
The contract states a setting-out envelope before production starts. If the as-built piers fall outside it, remediation is scope-side and we will quote it, but the more common outcome is that a survey catches the deviation while the piers are still open. Our payment draw schedule guide explains how the repair window is funded without disrupting the module programme.
Do we have to choose liquid cooling at design stage?
You have to decide the rack density envelope, which in practice decides the cooling architecture. Designing for 45 kW and installing rear-door heat exchangers first is a legitimate staging strategy, provided the structural load allowance and the manifold provisions are built in from the start. Retro-fitting liquid distribution into a hall built for air is the expensive version of the same decision.
How does factory construction affect the commissioning schedule?
It moves most of the testing earlier. Integrated systems testing at the factory happens while site works are still running, so the site phase carries less unproven equipment. The practical effect is a shorter site programme, but it requires the client's commissioning agent to attend the factory test, and that attendance has to be scheduled rather than assumed.
What is the realistic delivery time for a 20 MW AI campus?
Roughly 8 to 10 months from frozen design to first IT load, against 14 to 18 months for a comparable site-built programme. The saving comes from overlapping factory production with site works, not from working faster. If the design is not frozen before production starts, the overlap disappears and so does the schedule advantage.
Who is responsible if a module arrives damaged?
Risk transfer should be defined by stage rather than by asset, and the boundary that causes disputes is the crane lift. We define handover at the point the module is landed and set, not when it leaves the factory, because transport and lifting are the two operations where damage actually occurs and both are best managed by one party. Our contract types comparison sets out the three structures buyers normally choose between.
AI infrastructure decisions are made in weeks, not months. Modular construction is the only delivery method that matches that decision velocity.