Both modular construction and conventional steel frame construction start from the same material. Both use structural steel. Both comply with the same building codes, IBC, AISC 360, local amendments. But from that shared starting point, the two methods diverge so dramatically that a developer choosing between them is effectively choosing between two different industries: one that builds inside a factory, and one that builds in a field. This comparison examines every dimension that matters to project outcomes: timeline, cost structure, quality control, design flexibility, fire safety, seismic performance, and long-term building value.
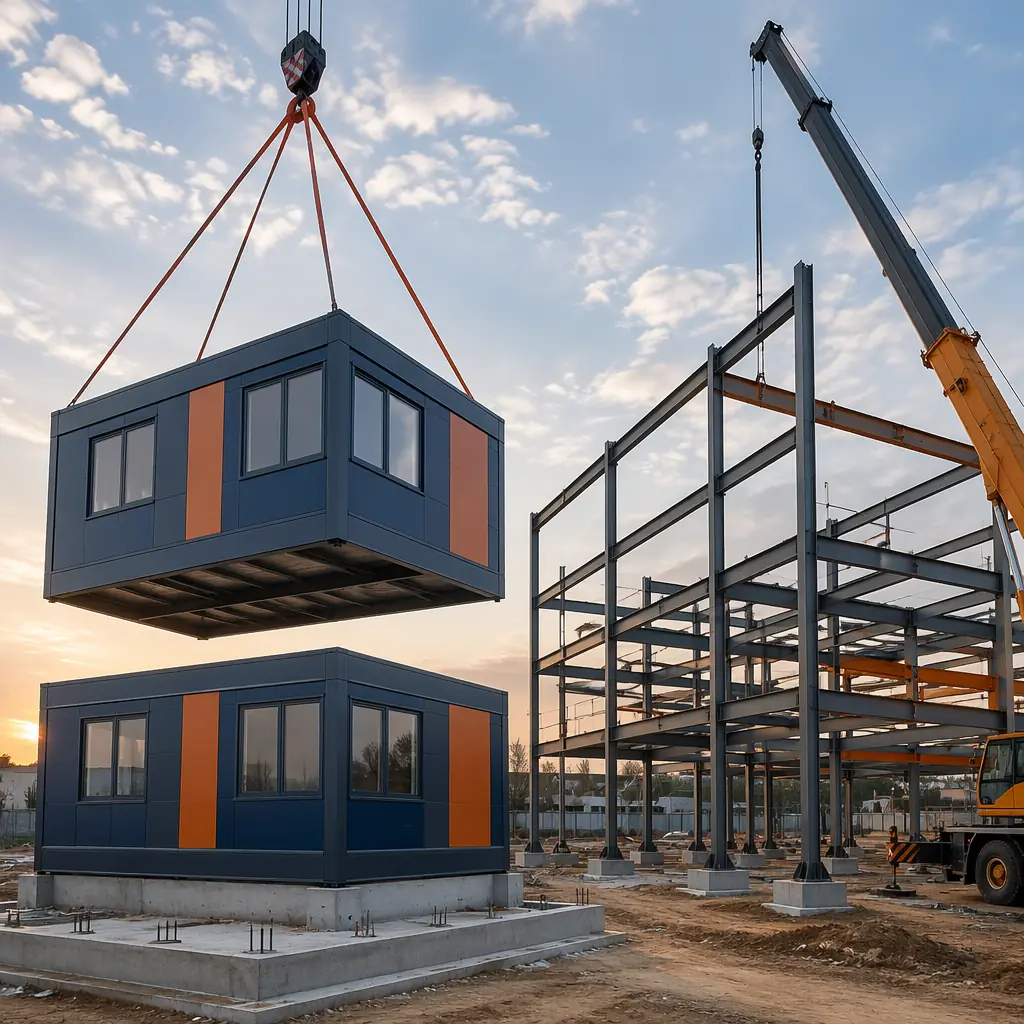
Where the Steel Goes, Factory vs Field Assembly
The critical distinction is not what material is used, but where it is assembled. In conventional steel frame construction, raw steel members, wide-flange beams, HSS columns, channel sections, arrive at the site as individual pieces. A steel erection crew connects them in the open air, working from mobile cranes and man lifts, exposed to wind, rain, and temperature extremes. The work proceeds sequentially: columns first, then beams, then decking, then fireproofing, then the building envelope can begin. Each trade waits for the one before it to finish before it can start. A 50,000 sq ft commercial building typically spends 14–20 weeks in this structural steel phase alone.
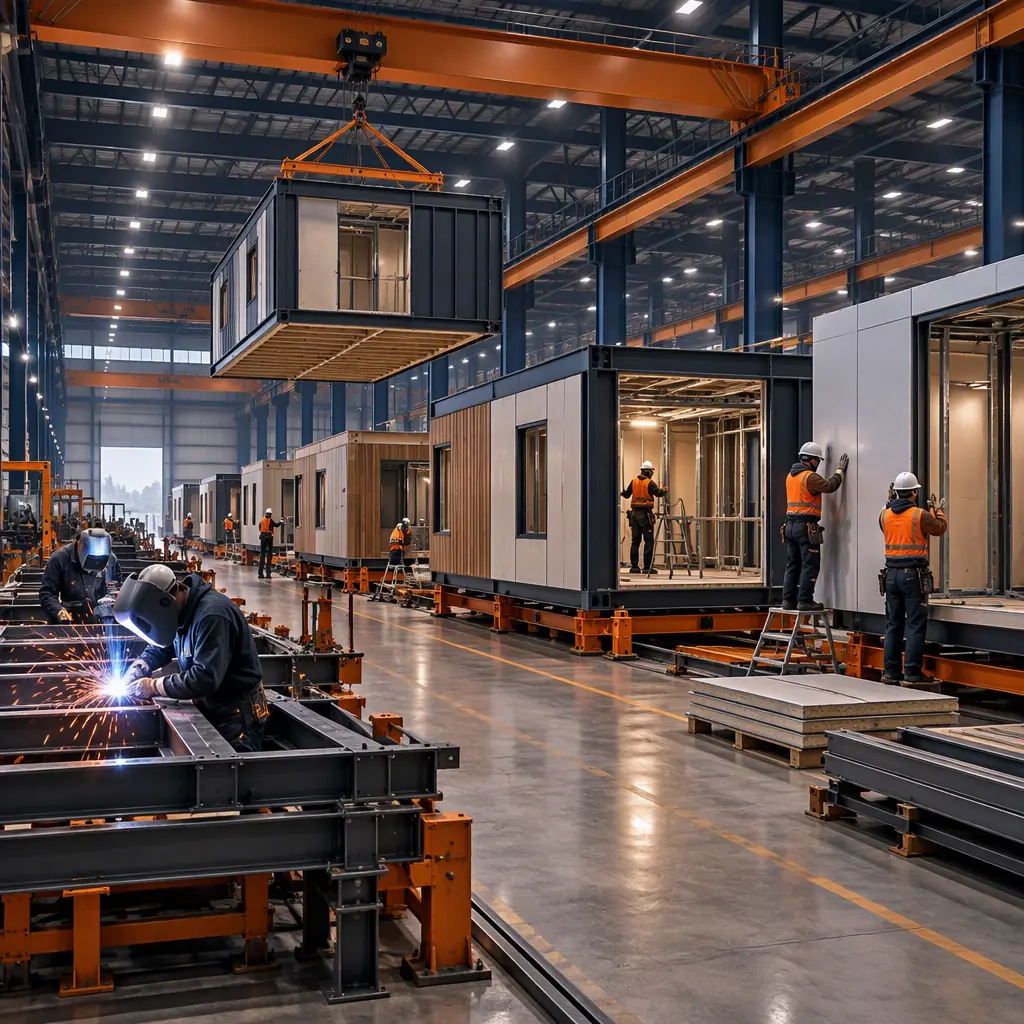
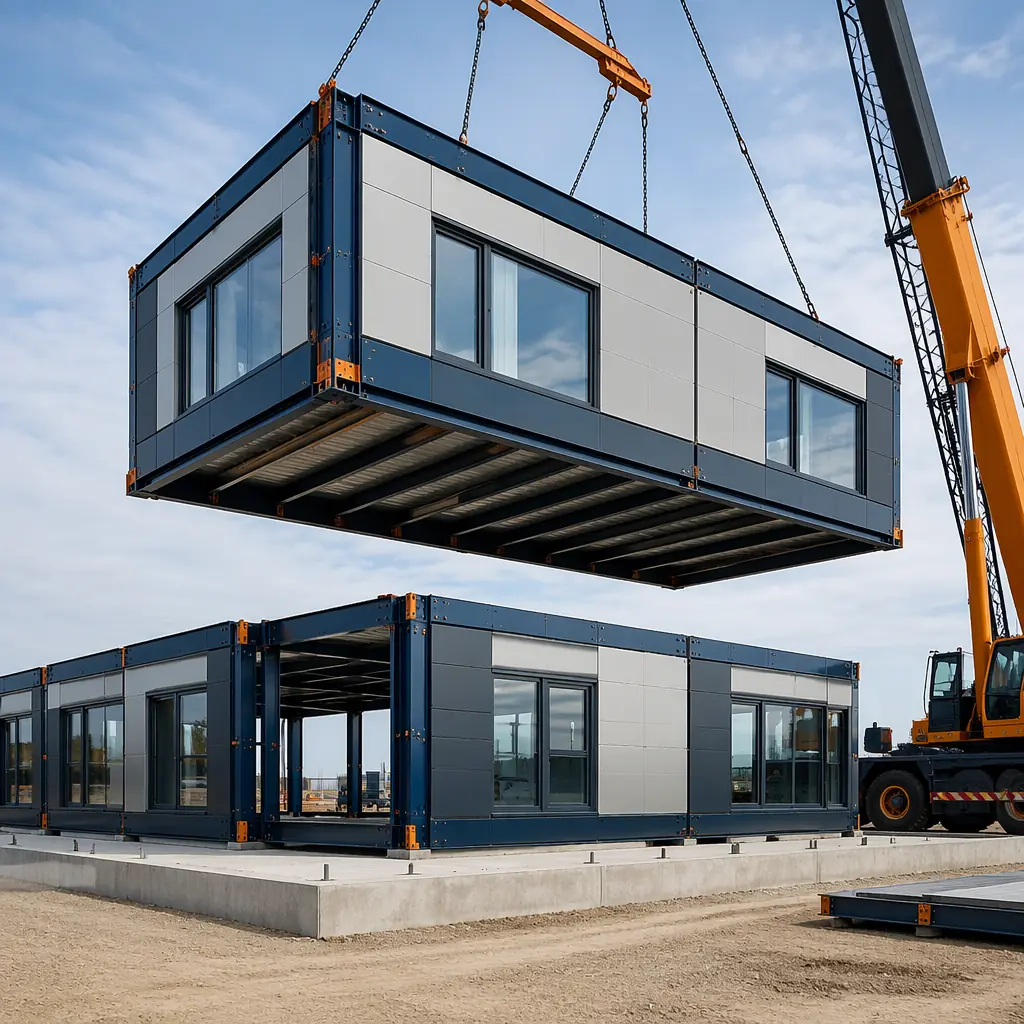
In modular steel frame construction, the same steel shapes are cut, welded, and assembled inside a factory, but they become part of a completed building module, not a bare frame. The steel frame of a module is fabricated on a production jig that guarantees dimensional accuracy to within ±2 mm across a 14-meter module length. Wall panels, windows, plumbing stacks, electrical conduits, and interior finishes are installed while the module is still on the factory floor, under roof, with QA inspectors checking every weld and connection. By the time a module leaves the factory, it contains 85–95% of its total labor content. The site crew connects modules together rather than building from raw steel.
This factory-to-site transfer is what produces the speed advantage that developers consistently rank as modular's number-one benefit. For the developer who has already examined modular vs traditional construction timelines, the steel frame comparison is particularly instructive: both methods use steel, but modular uses it 40–60% faster.
Scope Split at the Module-to-Frame Interface
The comparison above is decided on paper long before anyone picks a method. What actually decides whether a hybrid or fully modular steel project runs smoothly on site is a single question most method comparisons never ask: who owns the seam where the factory-built module meets the site-built steel? On a typical 8-storey hybrid, that seam is a few hundred millimetres wide and carries more contractual risk than the other 99% of the building. It is worth setting out explicitly, because the party who owns it is rarely the party who assumes they do.
| Interface Element | Who Normally Owns It | What Decides the Boundary |
|---|---|---|
| Module primary structure | Module manufacturer | Delivered to a set-out position, welded and inspected on a jig under ICC-ES ESR-5348 |
| Field splice between modules | Site erector, to the manufacturer's connection detail | Whether the bolted splice is a specified design element or left to site judgement, which is where it usually goes wrong |
| Fire stopping at the joint | Usually nobody, until it is caught at inspection | Whether the fire-rated assembly was tested as a system that crosses the joint, or as two panels that meet at it |
| MEP continuity across modules | Site MEP contractor | How much of the connection is pre-terminated in the factory and how much is left as a live tie-in |
| Weather seal at the module line | Envelope subcontractor | Whether the joint detail is a gasketed dry joint or a site-applied wet seal, which determines who returns when it leaks |
| Tolerance closure | Module manufacturer, if the set-out is theirs | Field tolerance on a site-built frame is typically ±6 mm against ±2 mm on a factory jig, so the frame, not the module, absorbs the difference |
The row that breaks projects is fire stopping. It is the only element in the table that is genuinely nobody's, because it exists only in the space between two scopes, and it is the element a building inspector will find. The practical fix is procedural rather than technical: name one party as responsible for the complete joint assembly, and make the fire-rated test evidence cover the assembly as built on site, not as tested as a panel in a laboratory. For hybrid programmes where the interface is genuinely complex, the same discipline used on modular versus PEMB scope splits applies directly: every line of the seam gets one owner and one witness.
Cost Structure Comparison, Where the Money Goes
The cost difference between modular and conventional steel frame is not a simple per-square-foot comparison. The two methods have fundamentally different cost structures, and the total project cost depends heavily on project type, location, and scale.
| Cost Category | Modular | Conventional Steel Frame |
|---|---|---|
| Structural steel material | $18–24/sq ft (factory bulk purchasing, optimized cutting) | $16–22/sq ft (project-by-project pricing) |
| Steel erection labor | $4–7/sq ft (factory assembly + 2–3 day site set) | $12–18/sq ft (14–20 weeks of site labor) |
| Fireproofing | $2–4/sq ft (factory-applied, QA-inspected) | $5–8/sq ft (site-sprayed SFRM, weather-delay risk) |
| General conditions / site overhead | $3–5/sq ft (compressed schedule) | $8–12/sq ft (extended site duration) |
| Total structural + erection | $27–40/sq ft | $41–60/sq ft |
The modular advantage in site labor and general conditions more than offsets its slightly higher material cost. For a 50,000 sq ft project, the structural cost difference alone can reach $500,000–$1,000,000. When factoring in the compressed schedule, which means earlier occupancy, earlier rent collection, and lower construction loan interest, the total project cost advantage typically widens further. Developers evaluating modular construction cost per square foot will find that factory-built steel consistently undercuts site-built steel on total project economics.
The Cost Lines Developers Forget to Price
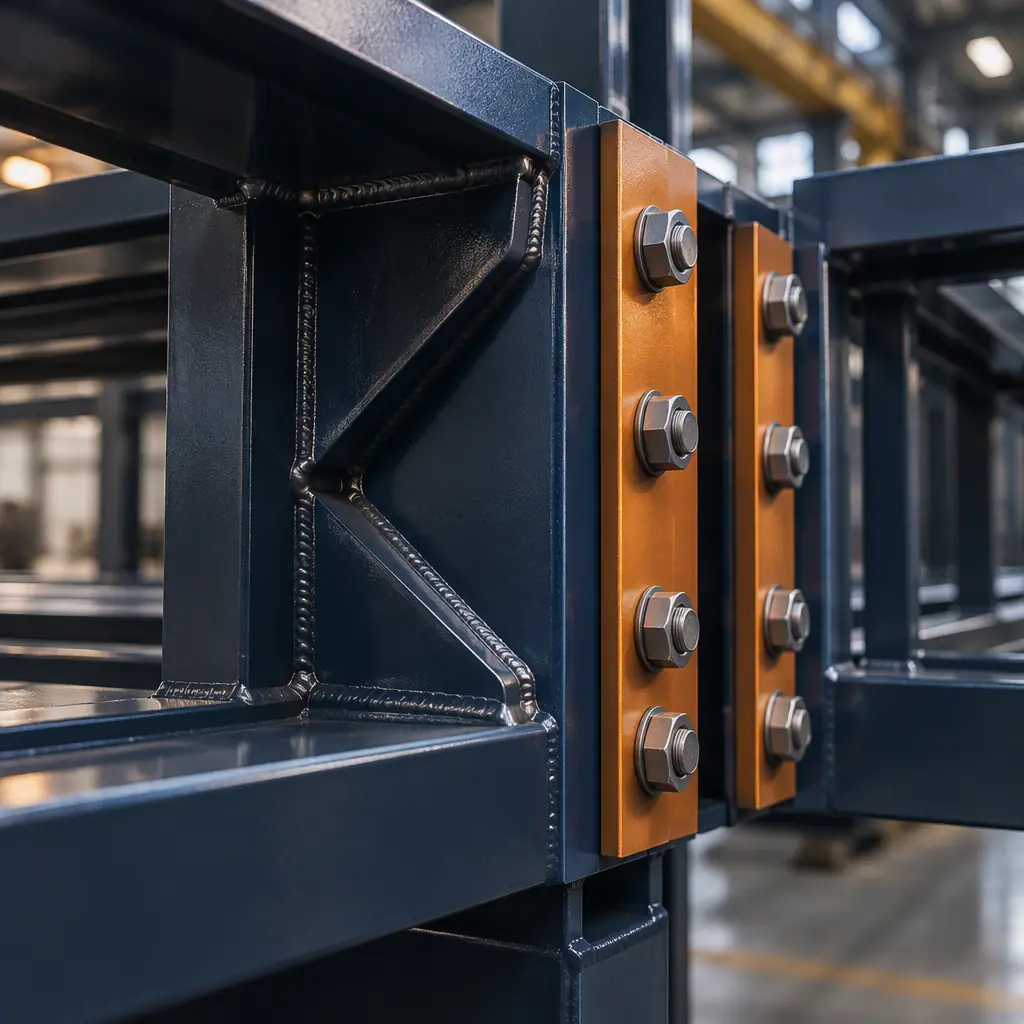
The structural cost table above covers the steel itself. It does not cover the five lines that decide the final number, and these are the lines that most frequently turn a steel frame comparison into a contract dispute. On a 50,000 sq ft hybrid commercial building, these secondary lines together run $4–9/sq ft, or roughly $200,000–$450,000, which is more than the entire structural cost advantage modular claims on the headline figure.
| Cost Line | Modular | Conventional Steel Frame | Why It Diverges |
|---|---|---|---|
| Erection interface extras | $1–2/sq ft (splice plates, packers, torque verification) | $3–5/sq ft (moment connections, field welding, NDT sampling) | Bolted splices on a jig-built frame need far less field welding, and welding is where the hours concentrate |
| Crane standing time | Compressed: modules set in 2–3 days per floor | Extended: 14–20 weeks of sequential steel erection | Crane hire is priced by the week, so a shorter erection phase is a direct saving, not a soft benefit |
| Interface defect rework | Low if the splice is factory-detailed | Highest single risk on the programme | A mis-set frame is corrected in mid-air on a crane; a mis-set module comes back on the jig |
| Temporary weather protection | Minimal: modules arrive clad and sealed | $1–2/sq ft of temporary sheeting and heating | An open steel frame is exposed for months; a set module is a closed envelope the day it lands |
| Post-set MEP tie-in | $1–3/sq ft of connection work only | Full first-fix install on site | Factory-installed conduit and risers reduce site first-fix to jointing, which is a smaller and cheaper trade package |
The honest reading of this table is that modular does not win on every line. Module freight is a real cost that a local steel mill does not carry, and for a project more than roughly 1,500 km from a production base, freight can consume the entire erection saving. The full cost-per-square-foot arithmetic is where that trade-off should be settled, not on the headline structural figure.
Warranty and Liability Stack at the Steel Interface
Steel frame comparisons rarely discuss what happens in year six, which is precisely when the consequences of the method choice surface. In a modular steel building the warranty obligations do not sit in one document, they stack, and the buyer needs to know which layer responds to which failure. The single most common dispute trigger on modular steel projects is a leak or crack at the module joint: the manufacturer says the splice was bolted to drawing, the erector says the drawing was wrong, and the waterproofing contractor says neither their scope nor their defect.
| Warranty Layer | Typical Holder | Typical Term | What Voids It |
|---|---|---|---|
| Module structural frame | Module manufacturer | 10–20 years structural | Third-party field modification of the frame; unapproved opening cut into a module chord |
| Field splice and connections | Site erector | 12–24 months workmanship | Missing or unsampled torque records; splice altered on site without engineer sign-off |
| Envelope and weather seal | Envelope subcontractor | 5–10 years, often manufacturer-backed | Movement at the joint exceeding the seal's design tolerance, which is a structural not an envelope fault |
| Fire-rated assembly | System supplier, tested to Intertek ISO 3008-1 | Life of the assembly if unmodified | Penetrations added after handover that were not part of the tested build-up |
| MEP connections | MEP contractor | 12–24 months | Restriction or blockage traced to a connection made across the module joint |
| Coordination failure | Nobody, by default | None | This is the gap. It is closed only by an explicit interface clause naming one owner for the completed joint |
The last row is the one to negotiate. A well-written contract names a single party responsible for the completed joint as a system, and requires that party to carry whatever warranty responds at that seam. Buyers who want the full picture of how these layers behave over a building's life should read the structural warranty and guarantees guide, and the insurance and risk-transfer analysis that covers what happens when the layers overlap.
Quality Control, Factory Precision vs Field Tolerance
This is where the two methods diverge most sharply, and where the consequences of choosing site-built steel become visible over the building's lifetime.
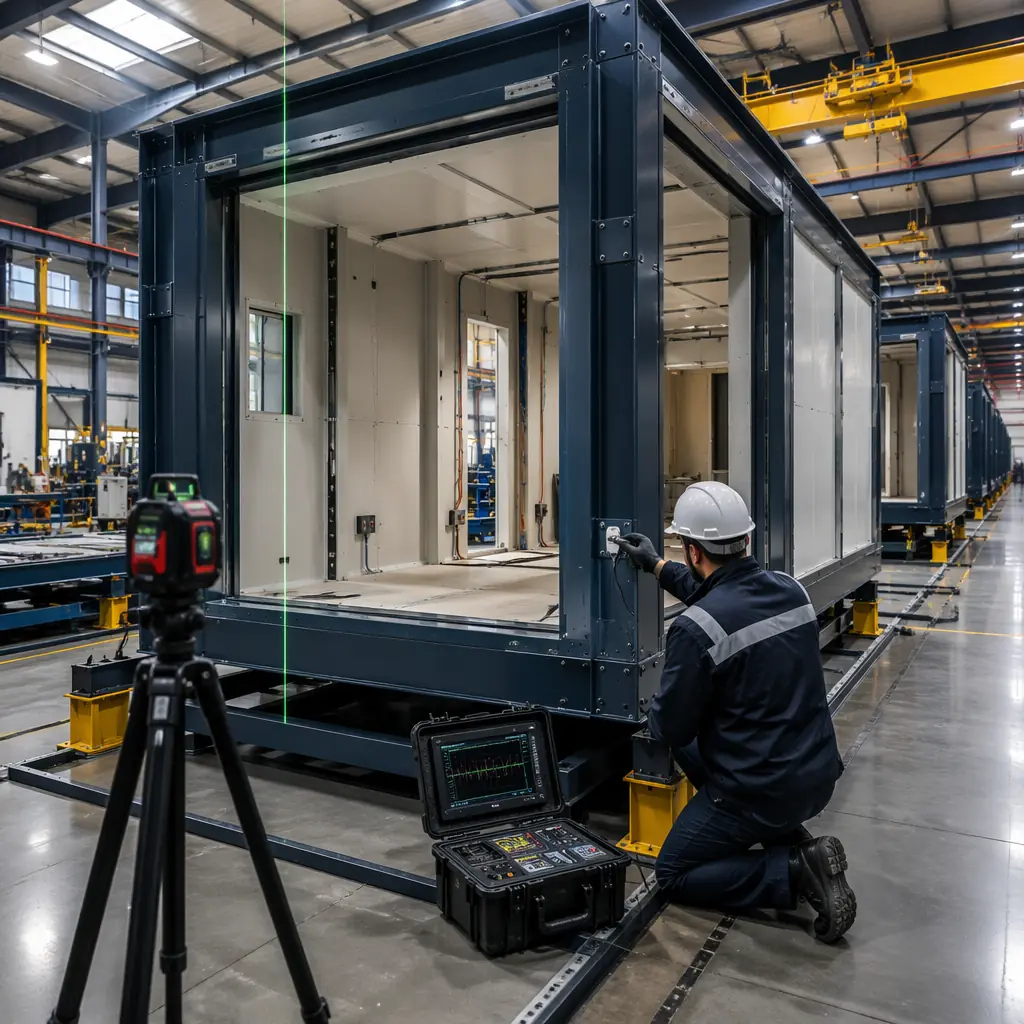
In the factory, every steel connection is welded on a calibrated production jig. Weld inspectors certified to AWS D1.1 examine every complete joint penetration weld using ultrasonic testing. Dimensional checks are performed at three stations: after frame welding, after wall panel installation, and before module shipment. The factory operates under an ISO 9001-certified quality management system with documented procedures, traceable material certifications, and audited inspection records. The environmental conditions are controlled: 18–25°C, low humidity, no rain on exposed steel.
On the conventional steel frame site, erection crews work from the drawings with field-measured dimensions. Column base plates are set in wet concrete with anchor bolt templates that typically achieve ±6 mm tolerance, three times looser than factory jigs. Field welding is weather-dependent: wind above 15 mph can blow away shielding gas on MIG welds, rain requires tenting, and cold weather requires preheating that is frequently skipped under schedule pressure. Field bolt tension verification is typically done by the "turn-of-nut" method rather than calibrated torque wrenches. Weld inspection is sampled: typically 10% of connections, rather than comprehensive. This is not because site crews are less skilled; it is because field conditions make factory-level precision physically impossible.
The consequences accumulate over decades. A factory-welded module frame with consistent 2 mm tolerances produces square corners that keep doors and windows operating smoothly for 30+ years. A field-welded frame with 6 mm variability produces cumulative racking that shows up as sticking doors, cracking drywall, and leaking window seals within 5–10 years. For developers who have invested in understanding modular construction warranties and structural guarantees, the quality-control argument for factory assembly is difficult to refute.
Fire Safety, Both Methods Meet Code, But Differently
Both modular and conventional steel frame construction achieve required fire resistance ratings, but through different mechanisms that affect cost, construction sequence, and long-term durability.
Conventional steel frame fire protection typically uses spray-applied fire-resistive material (SFRM), a cementitious or mineral-fiber coating sprayed onto steel members after erection. Achieving a 2-hour rating requires approximately 40–50 mm of SFRM thickness, applied in multiple passes with curing time between each. The application is weather-sensitive: high humidity slows curing, rain washes uncured material off, and cold temperatures require tenting and heating. The SFRM is fragile, it chips when struck by MEP trades working around the steel, and damaged areas must be patched, often without documentation. Over time, vibration from building use and building settlement can cause SFRM delamination in concealed ceiling spaces, where the damage goes undetected until a fire event.
Factory-built modular fire protection uses a fundamentally different approach. Each module's steel frame receives intumescent paint, a thin-film coating that expands to 50 times its dry-film thickness when exposed to fire, forming a char layer that insulates the steel, in a controlled spray booth with documented dry-film thickness verification. Alternatively, modules use factory-installed fire-rated gypsum board assemblies tested as complete systems at accredited laboratories. The fire-rated assembly is inspected and signed off before the module leaves the factory, with photographic documentation. Because the modules are 85–95% complete before site delivery, the fire protection is not exposed to weather, trade damage, or schedule-driven shortcuts. For developers building in jurisdictions with stringent fire code enforcement, modular construction fire safety documentation provides a level of verifiability that site-applied SFRM cannot match.
Seismic Performance, Ductility and Connection Design
Steel is inherently ductile. It can deform significantly before fracture, absorbing seismic energy through plastic deformation rather than brittle failure. Both modular and conventional steel frame construction exploit this property, but their seismic load paths differ in ways that affect performance in high-seismic zones.
A conventional steel moment frame resists lateral loads through rigid beam-to-column connections that transfer moment through the frame. The connections are designed to yield in a controlled sequence, beams yield before columns, connections yield before members, providing the ductility that modern seismic codes demand. However, the site-welded moment connections that make this work are among the most demanding field operations in construction: complete joint penetration welds in overhead positions, requiring prequalified welding procedures, certified welders, and ultrasonic testing. The 1994 Northridge earthquake revealed that even properly executed field moment connections can fail in brittle fracture modes that were not predicted by laboratory testing of idealized specimens.
Modular steel buildings resist seismic loads through a combination of module-to-module connections and dedicated lateral force-resisting systems. Each module is a rigid steel box with fully welded connections at every joint. The factory environment makes complete joint penetration welds routine rather than exceptional. Modules are connected to each other using high-strength bolts at the corners, creating a continuous load path from roof to foundation. In high-seismic applications, dedicated braced frames or shear walls are integrated into specific modules and connected across module joints. The result is a building with multiple redundant load paths. A characteristic that seismic engineers value because redundancy prevents progressive collapse if any single connection is damaged. For projects in seismic zones, modular seismic design provides specific connection details and testing data that demonstrate how factory-welded steel frames perform under cyclic loading.
Which Projects Should Choose Which Method?
| Project Characteristic | Better Fit: Modular | Better Fit: Conventional Steel Frame |
|---|---|---|
| Repetitive units (hotels, apartments, dorms) | ✓ 40–60% faster, 25–35% lower cost | No advantage |
| Large clear-span spaces (warehouse, gym, atrium) | Possible but module-to-span ratio increases cost | ✓ Optimized for long spans with deep beams/trusses |
| Tight urban site with limited laydown | ✓ Just-in-time delivery, minimal site storage | Requires laydown area for steel deliveries and staging |
| One-off architectural landmark | Higher design cost for unique module configurations | ✓ Unlimited architectural freedom |
| Schedule-critical (revenue-dependent) | ✓ Factory + site work overlap cuts 30–50% from schedule | Sequential workflow, weather-dependent |
| Builder in remote location (labor shortage) | ✓ Factory labor pool independent of site location | Depends on local skilled ironworker availability |
When Hybrid Makes Sense
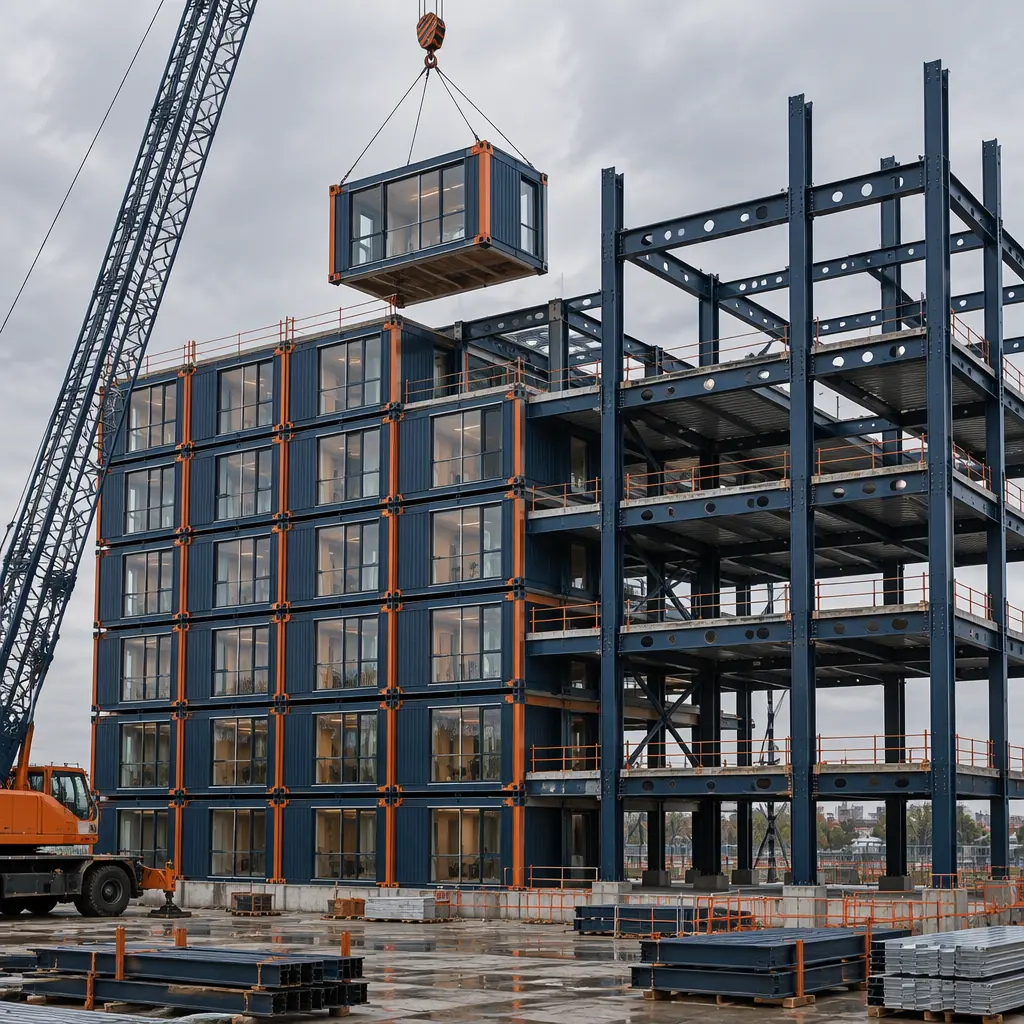
Not every project requires a binary choice. The most sophisticated developers are increasingly using modular for the repetitive program elements, guest rooms, patient rooms, apartment units, office suites, and conventional steel frame for the unique program elements, lobbies, atriums, conference centers, restaurant spaces. This hybrid approach captures modular's speed and quality advantages for 70–85% of the building area while preserving architectural freedom for the spaces that define the building's identity. The key to successful hybrid projects is early collaboration between the modular manufacturer and the steel frame contractor to coordinate module-to-frame connections, fire-rated separation, and MEP continuity across the interface. Projects using this approach have delivered at 20–25% below the cost of all-modular and 15–20% faster than all-conventional, according to developers who have shared data on modular construction ROI from completed projects.
Programme Milestones and Hold Points for a Steel Frame Decision
The speed claim in this comparison is only meaningful if it survives an actual programme. For a 120-unit mid-rise modular steel building, the milestone sequence below shows where modular compresses, where it does not, and which hold point gates the next phase. The compression is real but it is front-loaded: modular buys time by overlapping factory and site work, and it loses some of that back in the approval and transport window that a site-built frame does not have.
| Milestone | Modular (month) | Conventional Steel (month) | Hold Point That Gates It |
|---|---|---|---|
| Design freeze | 2–4 | 4–7 | Module repetition confirmed and every unit type signed off; a later change costs a jig reset, not a drawing revision |
| Foundation complete | 4–6 | 5–8 | Pad set-out surveyed to module plan; a foundation built to the wrong grid stops the first delivery |
| Structure starts | 4 (factory, overlaps foundation) | 8 (site, waits for foundation) | Factory slot booked; production capacity, not the site, is the constraint |
| First module set / first steel raised | 6–8 | 9–12 | Crane and transport slot confirmed; the interface connection detail is issued and approved |
| Weathertight | 9–11 | 15–20 | Joint sealing and fire stopping completed and witnessed across every module line |
| MEP and fit-out complete | 11–13 | 19–26 | Cross-module services tested as a continuous system, not per unit |
| First revenue | 13–16 | 24–30 | Occupancy certificate; the whole point of the compression is that rent starts here |
On a 120-unit building at a conservative $1,400 per unit per month, the nine-to-ten month gap between modular and conventional first revenue is roughly $1.5 million of rent brought forward, against which the freight and early-commitment costs of modular have to be set. That is the calculation the developer ROI guide works through in full, and it is also why the milestone table matters more than the headline speed percentage.
What We Decline to Take On
A comparison written by a party that sells one of the two options is worth exactly as much as its willingness to state what it will not do. Four things MODURA will not accept on a steel frame programme, because taking them on would transfer a risk we cannot control to a client who cannot see it:
- An unnamed interface responsibility. If a contract cannot name the single party who owns the completed joint between module and frame, we do not sign it. The risk is not the work, it is the gap, and the gap has no owner by default.
- Site erectors we have not vetting-approved. The bolted splice is straightforward but unforgiving. An erector without documented torque-verification records is a warranty problem in year three, not a saving in month six.
- Bespoke clear spans beyond the panel capacity. If a programme needs a long clear span that forces the module size above what our Q355B frame and panel build-up are tested for, the honest answer is conventional steel for that element.
- Retrofit into an occupied steel frame. Setting modules into a live building means field welding next to people and existing services, with no ability to control tolerances. We hand those to a specialist who does nothing else.
The same discipline applies to the services that cross the joint. Where MEP runs across module connections, we require the tie-in to be tested as one continuous system, which is the principle set out in the MEP systems integration guide. For heavy industrial programmes with unusual steel quantities or spans, the trade-off shifts again, and the heavy industrial steel comparison is the better starting point than this page.
Modular and conventional steel frame are not competing materials, they are competing production systems. The same ASTM A992 steel goes into both. But in modular, it arrives as a completed building. In conventional steel frame, it arrives as raw members. The decision is not about steel quality. It is about whether you want your steel assembled under a roof or in a field.
 Questions We Are Asked Before Every Steel Frame Comparison
These are the six questions that come up in almost every steel frame versus modular conversation, with the direct answer rather than the sales answer.
| Question | Answer |
|---|---|
| Is a modular steel frame as strong as a site-built one? | Yes, and the steel is the same grade. The frame is Q355B structural steel under an ICC-ES ESR-5348 listed light-gauge framing system, with connections fully welded on a calibrated jig. The difference is not strength, it is where the welds happen. |
| Who inspects the field splices? | The site erector, to a connection detail we issue, with torque verification recorded and witnessed. Weld inspection on the factory side is to AWS D1.1; the field side is bolted. Details of the factory-side regime are in the factory QC systems guide. |
| What happens if the foundation is out of tolerance? | The frame absorbs it, not the module. Field tolerance is typically ±6 mm against ±2 mm on the jig, so the set-out is surveyed before delivery and packers close the difference. A module is not designed to be forced onto a mis-set frame. |
| Does modular cost less per square foot? | On the structural and erection lines, yes, roughly $27–40 against $41–60. On the whole building it depends on freight distance and programme value. Beyond about 1,500 km from a production base, freight can consume the difference. |
| Can we mix modular and conventional steel? | Yes, and it is usually the right answer for a building with repetitive and unique elements. It requires the interface to be designed and owned explicitly. See the scope split above. |
| What certification backs the structure? | Production under ISO 9001:2015 / ISO 14001 / ISO 45001; structural system listed under ICC-ES ESR-5348; light-gauge framing certified to SGS CPR EN 14350; fire-rated assemblies tested to Intertek ISO 3008-1; steel to Q355B with CQC certification. Nothing in this list is estimated. |
For projects in seismic zones, the connection detailing needs its own conversation, covered in the seismic design guide. For low-rise buildings where a steel frame is simply the wrong method, the modular versus ICF comparison is a more useful read than this page.
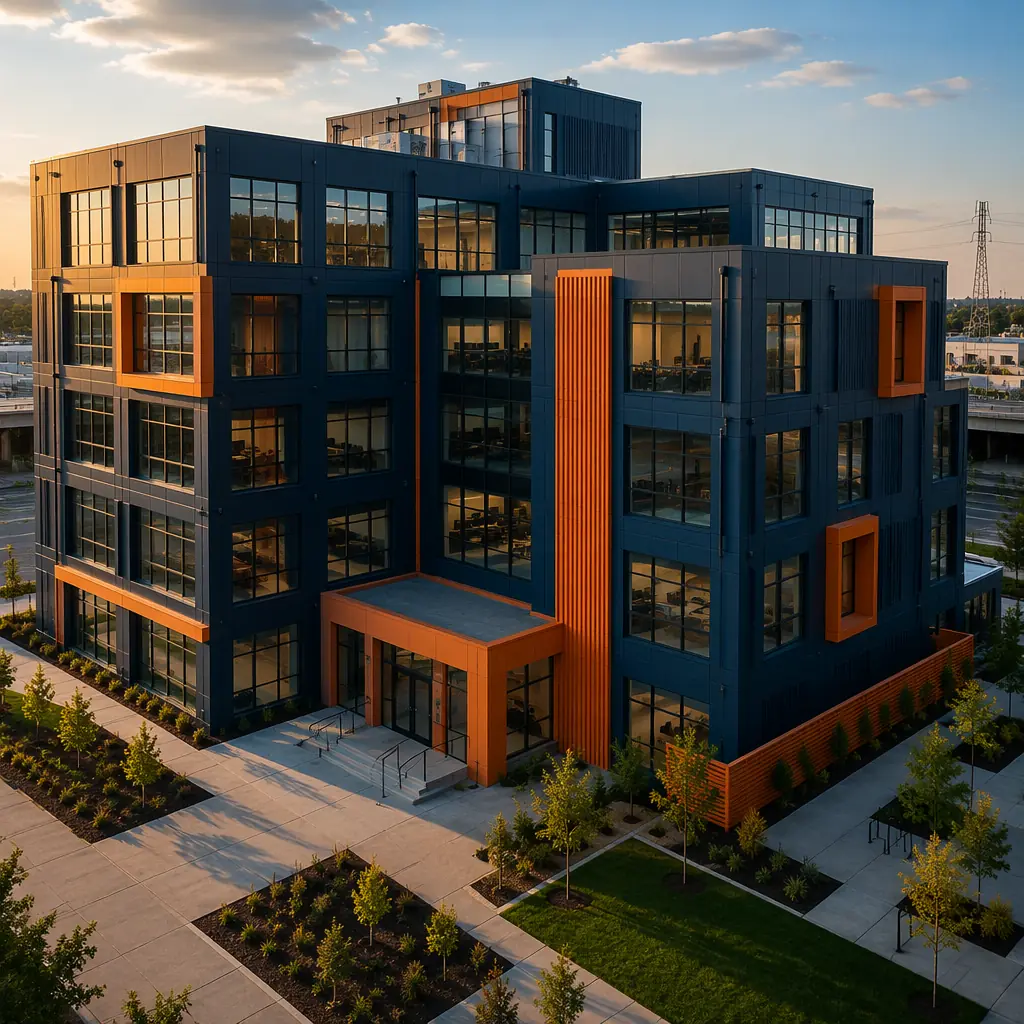
alt="Aerial view of completed modular steel frame multi-story commercial building complex, clean geometric facade showing grid pattern from factory-assembled modules, modern prefabricated construction, landscaping complete, dark navy structural design with warm steel orange brand accent details on building entrance, professional architectural photography" loading="lazy">